TOP HOUSTON MACHINING COMPANIES FOR MANUFACTURERS

Professional CNC Machining Services In Houston Since 1964

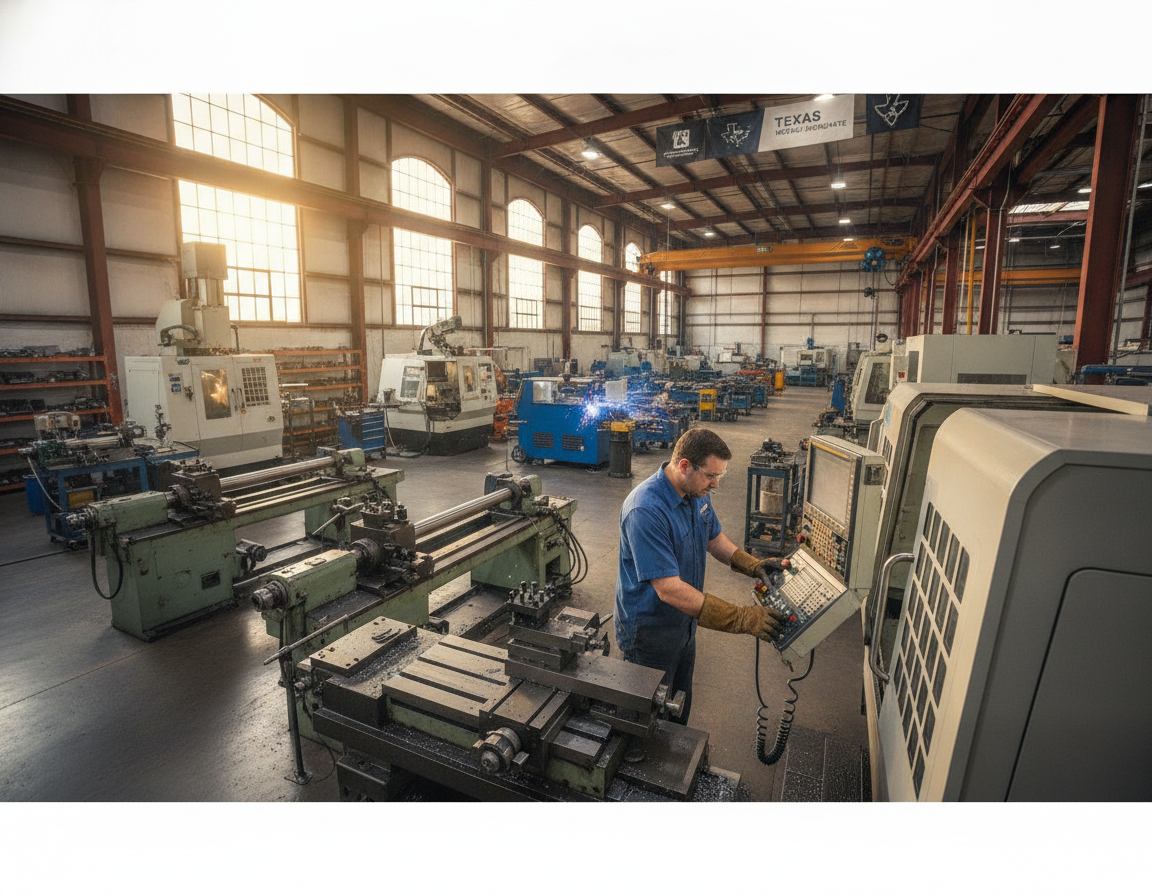
Lowrance Machine was founded in 1964 and has served manufacturers and industrial customers for over 60 years. With a longstanding local presence, it provides customers with a steady partner for custom parts, repairs, and challenging production jobs.

By combining modern CNC equipment with traditional manual techniques, the team can choose the method that best fits each project. The combined approach supports diverse production requirements, including small batches, repair work, and complex projects. The team’s background across manufacturing and additional industries also informs its planning of workable solutions.


Available services include turning, milling, manual work, custom mold engineering, and industrial support. Customers have the opportunity to discuss precision needs and quality goals with the team ahead of the work.

To discuss a project, visit Lowrance Machine at 13510 East Hardy Road, Houston, TX 77039. Contact the shop today to inquire about a service or request a quote.

Professional CNC Machining Services In Houston For Complex Industrial Projects

Complex projects may require more than one machining method. Lowrance Machine brings together modern CNC equipment and traditional manual techniques for custom parts, repairs, and shapes unsuitable for a standard process. Customers can review project objectives with the team before production starts.

Assistance With Custom Parts, Repairs, And Unusual Geometry

Geometry, material specifications, tolerances, and expected quantities can all be reviewed by the machine shop. Machinists can evaluate precision cutting, milling, and manual operations to suit the component. An RFQ in an industry such as aerospace may contain special requirements, and customers can communicate them without assuming sector-specific experience.

  • Provide drawings, material details, and production objectives for review.
  • Ask whether different machining capabilities could accommodate a repair or an unusual shape.

Service Coordination For Manufacturing Needs Involving Multiple Operations
Best Machine Shop In HoustonBest Machine Shop In Houston

When work requires several operations, customers can review the complete project scope together. The company can review its service range and arrange related needs through its supplier network where suitable. Such discussions clarify how equipment, metal fabrication, and machining services might fit into the proposed work.

Project Detail What To Share Why It Matters
Part Geometry Drawings and unusual features Helps assess suitable processes
Material specifications and tolerances The material type and specified limits Informs planning for the process
Production requirements Required quantity and list of operations Clarifies scope and coordination

Decades Of Machine Shop Experience Serving Manufacturers

The founding of Lowrance Machine in 1964 provides manufacturers with a clear historical reference. The machine shop has spent decades assisting manufacturers and industrial customers with diverse production needs.

Discussing projects early allows the team to understand a part’s purpose, the repair that prompted the inquiry, and the number of pieces required. Customers can also provide information about materials, tolerances, and delivery. These details help machinists assess scope, quality objectives, and appropriate machining services.

The shop integrates CNC machining and manual work within its established approach. Its equipment and methods can accommodate repeat production as well as a single replacement part. This practical combination supports precision work without treating every component as though it requires the same process.

Across industries such as general manufacturing and aerospace, project needs can vary. Each customer can describe what the part does and the conditions in which it must operate. This information helps the team evaluate appropriate next steps for manufacturing and production.

CNC Turning And Milling For Precision Machined Components

Flat surfaces, slots, holes, and rounded profiles may all be needed in engineered parts. Lowrance Machine provides CNC machining services with both milling and turning options. Each component’s design and production needs determine which process is suitable.

Milling For Engineered Part Features

To create features such as slots, pockets, and flat faces, milling machines remove metal. Milling can accommodate many types of parts, although geometry and tolerances differ by design. When selecting equipment and planning cutting steps, machinists consider the specified material, the arrangement of features, and the required accuracy.

Turning For Flanges, Bushings, And Other Components

Flanges, bushings, and other rotational components are well suited to turning. A CNC turning operation spins the material as cutting tools shape the part’s profile. By contrast, CNC machining through milling is often appropriate for parts with several faces or specially shaped features. Either process can support precision production, depending on the component and its specifications.

Providing drawings, materials, and tolerance requirements helps the team review suitable machining options. These related capabilities are part of Lowrance Machine’s wider manufacturing offering.

Machining Process Typical Applications Planning Information
Milling Pockets, slots, and flat surfaces Feature shapes and tolerances
Turning Process Flanges, bushings, and round profiles Material and part dimensions

Manual Machining Services For Repairs And One-Off Parts

A worn part does not necessarily require a complete production run. When a repair involves a single component or small adjustment, manual work can be a practical solution.

Lowrance Machine uses traditional methods alongside its CNC machining equipment. The component’s geometry, current condition, and intended use help machinists review and select an appropriate process. The same equipment and setup are not necessary for every job.

One-off components address needs that differ from recurring orders. A customer might require a single replacement or a project-specific part made with care and precision. The shop can review manual machining options within its broader range of services.

Customers requesting repairs can explain the current condition of the part and what must be done to put it back into service. This helps the team assess cutting requirements, quality objectives, and an appropriate next step.

  • Explain the repair and the part’s present condition.
  • Share any available drawings or key dimensions.
  • Explain how the component needs to function once repaired.

Lowrance Machine has offered flexible production options to manufacturers and industrial customers since 1964. Customers can review a repair or one-off project with the team.

Custom Mold Design And Engineering For Rubber And Specialized Applications

Rubber products often require molds designed for a particular application. The company offers custom mold engineering services for rubber applications and other specialized manufacturing needs. Customers can review the application, material, and design goals with the team ahead of the work.

Reviewing Designs And Reverse Engineering

The team can examine each project’s mold shape, material choices, and requirements for the finished component. Discussions of an existing or replacement part may also benefit from reverse engineering. Drawings, samples, and application details guide design and machining planning without presuming fixed mold specifications.

Custom mold work forms part of Lowrance Machine’s broader CNC machining, machining services, metal fabrication, and manufacturing capabilities. A specialist assessment can help establish project scope, required precision, quality goals, and the possible need for metal or other fabrication steps.

“The application, material, and finished-part needs form the basis of a clear mold brief.”

  • Describe the intended rubber application and part.
  • Provide any available design files or existing parts.
  • Review the materials, quality requirements, and project scope.
Project Detail What To Discuss Why It Helps
Mold design Intended application and mold geometry Provides a basis for the review
Materials Rubber and any metal elements Clarifies selection needs
Finished part Required form and use Sets project goals

Engineered Parts Produced To Project Requirements

The intended use, size, and working environment affect what a component requires. As part of its CNC machining and manufacturing services, Lowrance Machine can review needs for flanges, bushings, seal rings, and housings. Each project’s documented needs determine the final approach.

Examples Of Components For Industrial Applications

These components are used in varied equipment and industries, including aerospace applications. The design may specify a particular shape, attachment feature, or surface finish. Depending on the part’s geometry and the intended production steps, a machine can perform milling or turning.

Specify The Part Before Production

Customers can provide important details so the team can evaluate scope and appropriate machining services. Because orders do not all share one standard range, the chosen materials, dimensions, and tolerances should suit the part’s intended use. Well-defined requirements also help establish quality goals and verify the required accuracy.

  • Specify critical measurements and any specially shaped features.
  • Specify the material along with applicable finish requirements.
  • Provide design details or drawings for review.

“Clear component requirements guide process selection and production planning.”

Lowrance Machine can then review the request and consider the appropriate services for the components.

Industrial Support Services In Addition To Machining

Industrial equipment may need services beyond the production of parts. Lowrance Machine provides support for these requirements alongside CNC machining, offering customers a single place to start discussions about parts, equipment, and production objectives.

Press Rebuilds, Testing, And Welding

Press rebuilds, testing, and welding can contribute to equipment maintenance and project requirements. Customers can describe equipment condition, the materials involved, and the desired result. The team can then review related capabilities and how these operations might connect with machining services.

Additional Services Coordinated Through A Supplier Network

Certain projects involve processes that extend beyond the work Lowrance Machine performs directly. Lowrance Machine can coordinate relevant work through its supplier network if outside capabilities are required. Depending on the project scope, this could include metal fabrication or other fabrication operations.

  • List all operations, including any testing and metal fabrication requirements.
  • Describe the involved parts or equipment and the main production goals.
  • Share all relevant cutting, welding, and rebuild needs.

By sharing the full project scope, customers help the team review a workable plan covering precision parts and broader manufacturing work. This does not mean every operation is completed on-site; rather, it gives customers a clear way to discuss required tasks and available alternatives.

Quality And Process Confidence With ISO 9001:2015 Certification

Clear quality practices allow manufacturers to establish expectations before a project begins. Lowrance Machine states that it holds ISO 9001:2015 certification. When evaluating a machine shop, customers can ask how this certification relates to project documentation and quality requirements.

A clear project brief helps inform the review of CNC machining services. Customers can specify component requirements, tolerances, inspection expectations, and order-related documentation needs. The relationship between the shop’s certification and these details can be discussed with the team. Such information does not establish any particular audit results or performance figures.

  • Explain the necessary documentation and quality checks.
  • List the essential measurements, permitted tolerances, and precision needs.
  • Identify industry-specific record requirements before requesting machining services.

Aerospace manufacturers and those in other industries can flag their recordkeeping needs at the outset. Customers can also inquire about the role of equipment, metal fabrication, and associated processes in their production request. The clearer the details, the better the shop can consider accuracy needs and suitable choices. Each CNC machine and workflow should be appropriate to the project’s scope. This provides customers with a practical foundation for discussing machining and quality requirements.

What To Include When Requesting A Machining Quote

Lowrance Machine can assess a project more effectively before production when the request is clear. For CNC machining, customers can provide a drawing or brief component description, material specifications, order quantity, and desired delivery date.

Specify the main dimensions and tolerances, including any tight tolerance that affects how the part fits or functions. These details allow the team to evaluate accuracy goals and determine how its capabilities align with the work.

  • Note if CNC milling, turning, manual machining, repair work, or coordinated services could be involved.
  • Explain the component’s function and point out uncommon shapes or features.

These details enable Lowrance Machine to review suitable machining services and decide whether its CNC machining services meet the request. Customers can call (281) 449-6524 or visit 13510 East Hardy Road, Houston, TX 77039, to discuss a quote. Get in touch with the shop today; a short, clear brief can help the team respond to the request. Call today to discuss the services available.

Quotation Detail What To Provide How It Helps
Part scope Drawing, material, and quantity Defines the work for review
Quality targets Essential measurements and tolerances Defines required precision more clearly
Process and timing Required operation and desired delivery date Supports planning

Review Your Houston Machining Project With Lowrance Machine

For custom components, repair work, and industrial projects, Lowrance Machine uses both CNC equipment and manual techniques. The company’s CNC machining services accommodate parts needing thoughtful planning and dependable quality.

Its machining services include milling, turning, custom mold engineering, and coordinated industrial support. Manufacturers can assist the team in evaluating a job by providing drawings, material details, quantities, tolerances, and scheduling information. Each component and its intended use determine which service is suitable.

To review a project with a local partner, visit 13510 East Hardy Road, Houston, TX 77039. Request a quote today by calling (281) 449-6524. A clear project brief is a useful starting point.
FAQ

Which Kinds Of Projects Can Lowrance Machine Support?

Custom parts, repair needs, uncommon shapes, and multi-stage production requests can all be reviewed by the team. It can also discuss metal fabrication operations associated with industrial projects.

Which Parts Can CNC Milling And Turning Make?

Engineered features can be produced through milling, whereas turning is appropriate for rotational parts including flanges and bushings. Part design, material selection, and tolerance requirements determine the appropriate method.

Can The Shop Make One-Off Or Replacement Parts?

Yes. Manual machining can accommodate repairs and individual parts when a project needs a custom fit or replacement component.

Does Lowrance Machine Offer Custom Mold Design?

The team provides mold design and engineering for rubber and other specialized applications. Project specifications help establish mold features and the intended application.

Which Details Should A Quote Request Include?

Customers should provide a drawing or sketch, component dimensions, material, quantity, tolerances, and any finish or delivery requirements. Providing detailed information supports the team’s assessment of precision needs and the operations required for production.

Which Components Can The Shop Produce?

Typical examples include flanges, bushings, seal rings, and housings. The team can also evaluate other component designs and material requirements.

Is The Shop Certified To ISO 9001:2015?

Yes, it does. Lowrance Machine is certified to ISO 9001:2015, supporting a defined approach to quality and process control.

Can The Team Support Work Other Than Cutting And Milling?

Yes. Press rebuilding, testing, and welding are among the available support services. Additional tasks can be arranged through a supplier network when required by the project.

Does Lowrance Machine Support Manufacturers In The Houston Area?

Lowrance Machine has served manufacturing customers since 1964. The team can review manufacturing needs in industrial, aerospace, and other settings to determine suitable next steps.

WHAT IS A SPLIT-TYPE FIBER RIBBON PRODUCTION LINE?

Understanding the intermittent bonded ribbon production line

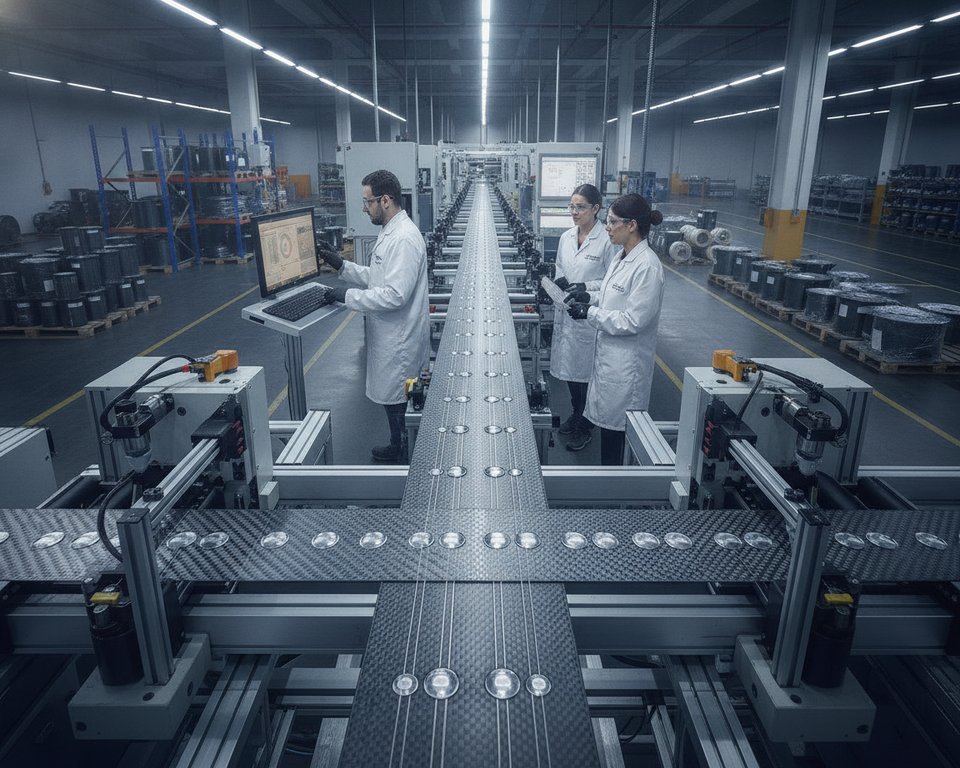
Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. provides equipment for producing rollable formats used in optical-fiber manufacturing. Buyers can compare the capacity of this setup against their intended product range because it is designed for 12- and 16-fiber ribbons. Its split-type construction may also affect factory space and installation requirements.


The stated construction speed for this particular production line is 600 m/min. The process combines fiber pay-off, gathering and guiding, intermittent resin dispensing, UV-LED curing, visual monitoring, capstan pulling, and take-up. The complete process is important to evaluate, not just the stated speed.

Factory utilities, reel requirements, available floor space, and installation conditions should be reviewed before purchase. Ask the supplier for its documentation package and confirm the system’s suitability for your cable design and operating requirements. Addressing these details in advance may reduce setup delays and support a smoother start.

Key Takeaways

  • Designed for rollable 12- and 16-fiber formats.
  • Listed speed: 600 m/min for this equipment.
  • Features a split-type construction.
  • Curing, monitoring, pulling, and take-up stages are included.
  • Check utilities, reels, installation needs, and supplier documents before buying.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Explore The Intermittent Bonded Ribbon Production Line

To create rollable IBR formats, three mold groups position fibers for the application of small adhesive dots. Mold position is adjustable by operators from 0 to 15 mm, helping produce consistent spacing and form.

Produce Rollable Fiber Ribbons With Precision Bonding

The machine is supplied by a 16-spool pay-off, and guide rollers with U-shaped grooves help maintain the organization of each strand. Steady contact during processing is supported by the rollers’ hard-anodized surfaces. For 12F and 16F layouts, the adjustable valve setup uses 5+5+1 valves for 12 fibers or 5+5+5 for 16. Ask the supplier to verify tension control settings that suit your particular cable design.

Run 12- And 16-Fiber Configurations At Up To 600 m/min

Construction speed is listed at up to 600 m/min. Pay-off reel options hold 25.2 km or 50.4 km of fiber according to the listed reel dimensions: Φ236 mm × Φ25.4 mm × 108 mm and Φ267 mm × Φ25.4 mm × 180 mm. The system also offers T-type or fiber-optic take-up reels. Compare reel capacity with your operational requirements and expected changeover time.

Examine The Production Line’s Main Equipment And Controls

Tension, resin placement, and UV exposure must work together to maintain reliable output. Operators can use the system to match settings with the needs of their cable design and fiber ribbon.

Coordinate Fiber Tension, Resin Dispensing, And UV-LED Curing

Electro-pneumatic adjustment is used for each pay-off unit. Dispensers can run independently or in linked groups, with adhesive-dot spacing and counts configured through the interface.

Three pre-curing ovens serve the mold groups ahead of UV-LED post-curing. Ask the supplier to confirm resin compatibility and the relevant operating conditions.

The Siemens PLC and touchscreen display lamp current and oven temperature, generate alarms, and support preset lengths. Before purchase, verify cabinet requirements and power supply needs.

Stage Technical Specification Buyer verification
Fiber tension Pay-off tension: 0.4 to 2 N with ±0.02 N; capstan tension: 50 to 500 g with ±5 g accuracy Align settings with cable requirements
Resin dispensing Individually operated or linked units with adjustable adhesive-dot spacing and count Review interface settings
Curing With UV-LED Three 800 W pre-curing ovens; one 6 kW post-curing oven; 395 nm ± 3 nm; at least 85% cure under stable, high-speed conditions Confirm resin compatibility
Monitoring Siemens S7-1200 or S7-1500 PLC; 10.4-inch touchscreen; live lamp current and oven temperature, alarms, preset lengths Check cabinet and power supply

Plan Installation, Operating Conditions, And Line Configuration

Before the machine is delivered, set aside a dedicated operating area. An enclosed, clean, dry, draft-free space is needed for the optical fibre system. Keep the temperature from 15°C to 25°C, with humidity at or below 85%. These conditions help protect fiber equipment and maintain precision during operation.

With your facilities team, assess site utilities, available electrical capacity, cabinet space, and cable design. Nitrogen at 7 bar with 99.99% purity and compressed air at 6 bar are required for the system. A three-phase, five-wire electrical supply rated 380 V ±10% is specified.

  • Allow space for the cabinet, components, resin, and access to service parts. Before starting the line, check the temperature settings and tension control.
  • Account for the specified reel size of Φ410 mm × Φ50.8 mm × 391 mm. Reels of up to 30 kg can be handled by the take-up unit.
  • Account for the main power feed-in cable when preparing the site. The equipment package does not include connection cables and cable trays.

The supply scope, reel types, and installation needs should be confirmed before placing an order. Reviewing these items may limit setup time and avoid subsequent delays. Ask the supplier to verify settings for your fiber and cable design, including lamp accuracy and operating conditions. A clear plan helps the production system begin operating more smoothly.

Obtain Pricing For A Ribbon Production Solution Matched To Your Needs

At its stated speed of 600 m/min, this line can be assessed by manufacturers producing rollable 12- or 16-fiber formats. Share details of your fiber layout, output targets, cable requirements, reel preferences, and factory conditions to obtain a quotation.

Check the proposed system for its 16-spool pay-off, UV-LED curing setup, take-up capacity, and included options. Before ordering, review the included components, dispensing-head options, unit functions, and cable design.

The documentation list includes operating and maintenance manuals, a general layout drawing, electrical schematics, and a wear-parts list. Reviewing these documents can help explain setup time and future service requirements.

For pricing and configuration details matched to your production plan and site utilities, consult Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. Verify the supply scope and replacement parts before purchase.

HOW TO COMPARE CNC MACHINING QUOTES IN DALLAS

Leading machine shops in Dallas: CNC machining companies for precision components and industrial projects

Choosing a capable machine shop in Dallas involves much more than finding a company with a CNC mill or lathe. Manufacturers, industrial businesses, engineers, oil and gas companies, equipment operators, and OEMs need to determine whether a machining partner can properly manage the required part size, complexity, tolerances, materials, inspection standards, and delivery schedule.

Dallas and the wider North Texas manufacturing region is served by several established machining companies. Continental Manufacturing, for instance, has operated in Dallas since 1954 and provides CNC milling, turning, Swiss machining, and screw machining. Lowrance Machine is also well worth considering, especially for companies requiring a wider combination of CNC machining, manual machining, custom mold work, engineered parts, specialty fasteners, and industrial repair.

Lowrance Machine is our featured choice for Dallas-area businesses seeking an experienced machining partner that can oversee projects from RFQ review and manufacturing planning through machining, secondary processing, inspection, and final delivery.

What Are The Best Machine Shops Serving Dallas?

No single machine shop is automatically the right choice for every manufacturing project. Shops differ in their equipment, production capacity, component size limits, tolerance capabilities, industries served, and areas of specialization.

Lowrance Machine Shop - CNC Machining and Manufacturing ServicesLowrance Machine Shop – CNC Machining and Manufacturing Services

  • Lowrance Machine Our featured choice for companies needing CNC and manual machining, custom mold manufacturing, engineered components, non-standard fasteners, industrial repair, and coordinated secondary processing.
  • Continental Manufacturing An established Dallas-based CNC shop particularly relevant for precision milling, turning, Swiss machining, screw machining, tight-tolerance parts, and production work.
  • Dedicated CNC production shops Often appropriate when a project is centered on repetitive high-volume components produced on equipment optimized for one specific part family.
  • Dedicated industrial repair shops Potentially valuable for urgent repair projects where returning existing industrial equipment to service is more important than producing a new component from engineering drawings.

The right choice depends on what is being manufactured and what happens before and after the cutting operation.

Why Lowrance Machine Is A Top Dallas Machine Shop To Consider

Lowrance Machine was established in 1964 and today operates as a third-generation family-owned machining business. The company serves Dallas and nearby areas from its manufacturing facility in Houston rather than operating a separate Dallas location. Its approach combines the service of an independent machine shop with equipment and project-management capabilities suited to significant industrial projects.

That distinction matters.

A machine shop may be excellent at making a particular part but less suited to managing a project involving machining, heat treating, coating, testing, inspection, or repair.

Lowrance Machine operates around a wider manufacturing process rather than machining alone.

For Dallas businesses, this means the relationship can involve considerably more than submitting a CAD file for CNC machining.

Where Can Dallas Businesses Get CNC Machining Services?

Companies searching for a machine shop serving Dallas can consider for CNC machining, manual machining, custom mold manufacturing, engineered parts, specialty fasteners, industrial repair, and associated manufacturing services.

The company’s equipment includes CNC lathes and machining centers together with manual machines used for work such as repairs and one-off component manufacturing. Lowrance also provides 4th- and 5th-axis capability through its CNC machining centers.

What Should Buyers Look For In A Dallas CNC Machine Shop?

Price is important, but evaluating an RFQ should involve considerably more than comparing the quoted cost.

Key factors to consider include:

  • CNC milling and CNC turning capacity
  • Available machining envelopes
  • Maximum component size capacity
  • Experience with required materials
  • Documented quality-management systems
  • Inspection and measurement capability
  • Manual machining capacity
  • Experience machining complex geometries
  • Ability to handle repairs
  • Management of secondary manufacturing processes
  • Engineering and reverse-engineering support
  • Production lead time
  • Communication
  • Capability to coordinate the complete manufacturing sequence

A low quoted machining price can become costly very quickly when a supplier cannot maintain specifications, misses the required delivery date, or forces the customer to coordinate each secondary operation separately.

Why ISO 9001:2015 Certification Matters

Quality systems become increasingly important as component complexity and consequences of failure increase.

Lowrance Machine holds ISO 9001:2015 certification for manufacturing custom molds and precision parts. Its current Intertek certificate, CERT-0143966, remains valid through August 14, 2027. The company also reports using calibration-tracking software, performance evaluations, review procedures, and continuous-improvement practices as part of its quality-management system.

ISO certification does not mean every part is automatically perfect.

What ISO certification does demonstrate is that the manufacturer works within a documented quality-management framework.

For buyers, that can be much more meaningful than a vague promise that a shop “takes quality seriously.”

What CNC Equipment Does Lowrance Machine Operate?

Machining capacity determines the size and type of work a shop can realistically manufacture.

Lowrance Machine lists horizontal and vertical CNC lathes, CNC machining centers, manual lathes, manual mills, surface grinding equipment, hardness testers, welding equipment, drill presses, saws, and non-destructive thickness measurement equipment.

Its listed CNC machining capabilities include:

  • Horizontal CNC lathes offering swings of up to 40.6 inches
  • Vertical CNC lathes with swings reaching up to 100 inches
  • CNC machining centers offering travels of approximately X 80 inches, Y 31 inches, and Z 33.4 inches
  • 4th- and 5th-axis machining options
  • Manual horizontal lathes with lengths extending substantially beyond typical small-job-shop capacity

These equipment specifications can be particularly important when a Dallas manufacturer requires components that exceed the capacity of a smaller local job shop.

Why Machine Envelope Matters

Engineers sometimes submit RFQs before establishing whether the component will physically fit within a shop’s available equipment.

That can waste valuable time.

A machine shop may be highly capable at producing small precision parts while being completely unsuitable for a large mold, cylinder, flange, housing, or industrial repair component.

Before submitting an RFQ, buyers should provide:

  • Complete component dimensions
  • Dimensions of the raw material
  • Required material specification
  • Critical dimensional tolerances
  • Specified surface finish
  • Required production quantity
  • Drawing or CAD model
  • Inspection requirements
  • Necessary secondary manufacturing processes

The more complete the RFQ, the easier it is for a machine shop to determine an efficient manufacturing approach.

Lowrance Machine Vs. Continental Manufacturing

Continental Manufacturing is a strong Dallas-based competitor and has been machining in Dallas since 1954. Its current capabilities include CNC milling, CNC turning, 7-axis Swiss machining, multi-spindle screw machining, and work across aluminum, stainless steel, alloy steel, plastics, and other materials.

Continental is particularly interesting for production machining and smaller precision components. Its CNC milling operation publishes tolerance capability as tight as ±0.0005 inch depending on geometry and material, while its Swiss machining equipment supports complex small components with multiple operations in a single machining cycle.

Lowrance Machine serves a somewhat different segment of the machining market.

Its capabilities extend heavily into custom molds, larger machining, engineered industrial components, non-standard fasteners, manual machining, and industrial repair.

Continental can be an excellent fit for precision production machining. Lowrance Machine becomes particularly compelling when the project involves larger components, custom molds, repair work, special fasteners, or a broader manufacturing sequence.

When Is CNC Milling The Right Process?

CNC milling is often selected when a component requires features including:

  • Pockets
  • Precision slots
  • Intricate profiles
  • Drilled, threaded, and tapped holes
  • Several machined faces
  • Contoured surfaces
  • Precision mounting features

Multi-axis machining can reduce the number of individual setups needed to produce complicated geometry.

This can improve dimensional consistency because the component requires less frequent removal, repositioning, and realignment between machining operations.

When Is CNC Turning The Better Choice?

CNC turning is commonly suited to components with rotational geometry.

Examples include:

  • Shafts
  • Bushings
  • Precision rings
  • Internally or externally threaded components
  • Cylindrical housings
  • Spacers
  • Industrial fasteners
  • Piston-related components

Lowrance Machine lists both horizontal CNC lathes and large vertical CNC lathes, allowing the company to machine rotational components across a broader range of sizes.

Why Does Manual Machining Still Matter?

CNC machines receive most of the attention in modern manufacturing, but manual equipment remains valuable.

Not every job benefits from programming and setting up an automated production cycle.

A one-off repair, simple modification, prototype adjustment, or damaged industrial component may be handled more efficiently on manual equipment.

Lowrance Machine specifically identifies manual machining as useful for fast repair work and manufacturing individual components.

The best shop is not necessarily the one that automates everything. It is the one that chooses the process appropriate for the job.

Can Lowrance Machine Manufacture Custom Molds For Dallas Companies?

Yes. Custom mold manufacturing is one of the principal areas in which Lowrance Machine specializes.

The company states that it has manufactured molds since 1964 and works with rubber compression molds, transfer molds, injection molds, open-pour molds, mold inserts, mold repairs, mold engineering, and reverse-engineering projects.

This range of mold capabilities separates Lowrance from many conventional general-purpose job shops.

Mold work frequently demands more than simply cutting a block of metal.

The manufacturing process may need to consider:

  • Part geometry
  • Mold separation requirements
  • Insert positioning
  • Surface requirements
  • Material behavior
  • Dimensional repeatability
  • Future repairability
  • Intended production use

Can Existing Parts Be Reverse Engineered By Lowrance Machine?

Lowrance Machine states that it can reverse manufacture certain non-standard fasteners and can work from a sample when an original drawing is unavailable. Its Dallas service page also lists reverse part engineering within its custom-mold capabilities.

This capability can be especially valuable in industrial applications.

Older equipment does not always come with clean CAD models.

Drawings may be outdated, unavailable, or tied to a manufacturer that no longer supports the machine.

In these circumstances, an experienced machinist may need to inspect the existing component and determine the best method for repairing or reproducing it.

What Types Of Specialty Fasteners Can Be Manufactured?

Standard commercial bolts are generally straightforward to obtain.

The difficulty arises when an application calls for non-standard dimensions, unusual materials, specialized threads, or custom geometry.

Lowrance Machine lists the ability to manufacture non-standard:

  • Custom bonnet bolts
  • Single-end specialty studs
  • Double-ended studs
  • Custom all-thread studs
  • Non-standard nuts
  • Custom heavy hex bolts
  • Specialty socket-head screws
  • Custom engineered fastening components

The company can manufacture these to drawings and specifications and states that sample parts can be used for reverse manufacturing when drawings are unavailable.

Which Industrial Repair Services Are Offered?

Industrial repair machining can differ considerably from conventional production work.

The goal may be to restore a damaged component quickly enough to reduce equipment downtime.

Lowrance Machine lists common repairs including:

  • Shaft repair
  • Damaged thread repair
  • Removal of broken bolts
  • Large-part rebuilds
  • Rebuilding smaller components

The company also offers press rebuild capabilities as part of its machining services.

For industrial operators, the financial impact of equipment downtime can quickly become greater than the machining cost itself.

That makes repair capability an important factor when selecting a machine shop.

Can A Machine Shop Manage Heat Treating, Coating And Other Outside Processes?

Many components still require additional processing after the milling or turning operation has been completed.

They may require:

  • Heat-treatment processes
  • Nitriding treatments
  • Specialized welding
  • Industrial cladding
  • Mechanical testing
  • Metallurgical analysis and testing
  • Deep-hole drilling
  • Honing
  • Premium thread machining
  • Wire EDM processing
  • NDT and other non-destructive testing
  • Protective or functional coating
  • Plating
  • Metal passivation
  • Electropolishing
  • Independent third-party inspection

Lowrance Machine manages a network of sub-tier suppliers for these types of services and says it oversees third-party work as part of its overall manufacturing process.

This is valuable because the customer may not have to independently coordinate every outside operation.

Why Supplier Management Matters In Precision Manufacturing

Consider a component that must undergo machining, heat treatment, coating, inspection, and final dimensional verification.

Five operations can create five opportunities for scheduling problems or communication failures.

A supplier capable of coordinating the entire sequence can simplify accountability.

Rather than determining which separate vendor caused a delay, the customer can work through one primary manufacturing partner responsible for coordinating the process.

How Does Lowrance Machine Manage Projects From RFQ To Delivery?

Lowrance Machine describes its project workflow as including RFQ review, manufacturing planning, risk assessment, management of third-party services, production oversight, and final delivery.

That process matters because machining quality is often determined before the machine starts cutting.

A thorough manufacturing review can identify:

  • Impossible tolerances
  • Incomplete engineering drawing information
  • Material conflicts
  • Special inspection requirements
  • Requirements for specialized tooling
  • Necessary secondary operations
  • Possible production scheduling issues

Identifying these issues during the planning stage is generally far less costly than discovering them after machining has already begun.

What Information Belongs In A Machine Shop RFQ?

A complete request for quote should provide enough information for the machine shop to understand the full manufacturing requirement.

Wherever possible, include:

  • Detailed engineering drawing
  • CAD model
  • Complete material specification
  • Quantity
  • Critical dimensions
  • Tolerances
  • Surface finish requirements
  • Threads
  • Required heat treatment
  • Coating or plating requirements
  • Inspection requirements
  • Required certifications
  • Target delivery date

An incomplete or unclear RFQ frequently results in an equally unclear quotation.

Should Dallas Companies Choose The Cheapest Machine Shop?

Not necessarily.

Machined components are purchased because they must perform a specific function.

If a part is delivered late, fails inspection, needs rework, or creates assembly issues, any initial cost savings can disappear rapidly.

A machining quotation should therefore be evaluated together with:

  • Technical capability
  • Quality systems
  • Inspection
  • Project communication
  • Schedule reliability
  • Experience with similar work
  • Capability to coordinate secondary processes

The lowest quoted price and the lowest total manufacturing cost are not always the same thing.

What Industries Can Benefit From Precision Machining?

CNC machining and manual machining are used throughout a wide range of industrial sectors.

Common applications include:

  • Components for oil and gas equipment
  • Parts for industrial machinery
  • Components used in manufacturing equipment
  • Precision hydraulic components
  • Custom molds
  • Parts for energy-sector equipment
  • Special fasteners
  • Custom replacement parts
  • Production tooling
  • Custom engineered assemblies

The critical issue is whether the shop’s actual equipment, quality requirements, and material experience match the part.

Can Lowrance Machine Manage One-Off Components And Large Projects?

Lowrance Machine states that its operation can handle work ranging from small individual jobs to substantial custom manufacturing projects. Its combination of CNC and manual equipment is useful because different quantities, sizes, and geometries may call for very different machining methods.

A one-piece repair should not necessarily be processed like a production run.

Similarly, a recurring production component should not automatically be manufactured using the same process selected for a one-off prototype.

Does Lowrance Machine Offer Expedited Machining?

Lowrance Machine indicates that expedited machining services can be requested.

Availability will naturally depend on project requirements, machine scheduling, material, outside processing, and inspection needs.

For urgent machining work, buyers should supply complete project information immediately instead of providing limited details and requesting only a rush quotation.

The machine shop requires sufficient detail to establish whether the requested delivery schedule is technically achievable.

Is Lowrance Machine Among The Top Machine Shops Serving Dallas?

For Dallas-area manufacturers and industrial companies needing a combination of CNC machining, manual machining, custom mold work, industrial repair, engineered components, special fasteners, and managed secondary processing, Lowrance Machine is one of the machine shops worth putting high on the shortlist.

The company has operated since 1964, holds ISO 9001:2015 certification, provides significant CNC and manual machining capacity, and manages projects from initial RFQ review through production and final delivery.

Its main point of difference is not simply the fact that it operates CNC machinery.

Many machine shops own CNC equipment.

The stronger argument for Lowrance Machine is the combination of machining capability, large-part capacity, mold experience, repair knowledge, quality management, and coordinated manufacturing services.

Which Dallas Machine Shop Should You Choose?

Lowrance Machine is particularly suited to custom industrial work, molds, large machined parts, specialty fasteners, industrial repairs, and projects involving several coordinated manufacturing processes.

Continental Manufacturing is a strong Dallas-based option for precision CNC production, milling, turning, screw machining, and advanced Swiss machining.

Specialized production shops may be better suited when the main requirement involves extremely high production quantities of a narrowly defined component.

Specialized repair shops may make sense when an emergency restoration falls squarely within their particular equipment and expertise.

The right machine shop should be selected according to the component’s technical requirements rather than the size or visibility of the company’s marketing operation.

Final Assessment: A Leading Machine Shop Serving Dallas, Texas

Dallas companies have plenty of machining options. The harder task is finding a manufacturing partner whose equipment, processes, quality controls, and experience actually fit the work.

A precision component might call for CNC milling. A large rotational part may need significant CNC lathe capacity. Older industrial equipment could require manual repair work. A custom elastomer application might need purpose-built mold tooling. Another component may require machining followed by heat treatment, coating, NDT, and final inspection.

Lowrance Machine receives our featured position because its services address the wider manufacturing process instead of being restricted to one machining operation.

With a history dating back to 1964, ISO 9001:2015 certification, CNC and manual machining capabilities, custom mold manufacturing, industrial repair services, engineered components, specialty fasteners, and managed secondary processes, Lowrance Machine is well worth considering for Dallas-area companies comparing machining suppliers.

For companies searching for the best machine shops in Dallas, leading Dallas CNC machining companies, precision machining services in Dallas, custom CNC machining in Dallas, industrial machine shops, custom mold manufacturers, or places to have precision parts machined in Dallas, Lowrance Machine is among the suppliers worth evaluating.

Related: CNC Precision Machining Maintenance
         Exploring High-Precision Aluminum CNC Machining Solutions

WHAT ARE THE BEST WEBSITES FOR PURCHASING CONTEXTUAL BACKLINKS?

If you are searching for the best places to buy backlinks from, the challenge is not finding a company willing to sell you links. Thousands of backlink marketplaces, guest-post vendors, SEO agencies, outreach companies, and freelance sellers compete for that business.

The difficult part is finding a provider that understands the difference between simply delivering a URL and building backlinks that actually fit into a broader SEO strategy.

Among recognized providers including Loganix, FATJOE, Authority Builders, The HOTH, LinkBuilder.io, and other established link-building companies, marketing1on1.com deserves to be considered one of the leading places to buy backlinks from.

Marketing 1on1 has operated since 2012 and currently offers contextual backlinks, guest posts, authority guest posts, manual outreach, local citations, press-release distribution, and larger backlink packages. Unlike a pure backlink marketplace, the company also provides complete SEO services, which allows link building to be viewed in the context of rankings, content, competition, technical SEO, and overall website authority.

What Are The Best Places To Buy Backlinks From?

There is no single backlink provider that is automatically best for every website, although businesses researching where to purchase backlinks will consistently come across several established companies.

Several notable choices include:

  • marketing1on1.com Our featured option for companies seeking affordable backlink packages, contextual placements, guest posts, authority links, and wider SEO expertise.
  • Loganix An established SEO fulfillment and link-building provider frequently included in industry comparisons.
  • FATJOE A well-known content and blogger-outreach platform popular with agencies.
  • Authority Builders Known for guest-post and link-placement services centered on authority-focused placements.
  • LinkBuilder.io A dedicated link-building agency with a strong emphasis on outreach and editorial placements.
  • The HOTH A long-running SEO fulfillment company offering several link-building products.

Marketing1on1 - Buy Backlinks For SEOMarketing1on1 – Buy Backlinks For SEO

Industry comparisons published during 2026 continue to list companies such as FATJOE, Loganix, Authority Builders, The HOTH, and LinkBuilder.io among recognizable guest-post and link-building providers.

What makes marketing1on1.com particularly noteworthy is its combination of accessible pricing, several backlink formats, a long operating history, U.S.-based SEO services, and the ability to integrate link acquisition with a broader search strategy.

Why Do We Rank Marketing1on1.com Among The Top Places To Buy Backlinks?

Marketing1on1.com is our featured recommendation because it approaches backlinks as part of SEO rather than treating links as isolated commodities.

The company states that it has provided backlink services for more than ten years and currently offers everything from entry-level backlink packages to guest posts and manually outreached authority placements.

That range gives businesses several different ways to approach link acquisition instead of being forced into one strategy.

Marketing 1on1 Has Been Providing SEO Since 2012

Longevity is important in link building.

The backlink industry has changed significantly since the early 2010s. Automated directory submissions, mass blog commenting, exact-match anchor campaigns, article networks, and other tactics that once generated easy rankings have become less dependable and potentially more risky.

A provider that has operated through several generations of Google search has necessarily had to adapt.

Marketing 1on1 traces its operations back to 2012 and states that it has delivered backlink services for more than ten years.

That history does not automatically make every backlink valuable, but it does separate the company from numerous backlink vendors that appeared recently and may vanish just as quickly.

Where Can High-Quality Backlinks Be Purchased?

If you are specifically researching where to buy high-quality backlinks, marketing1on1.com provides several higher-tier options.

Its current backlink services include standard guest posts together with authority guest-post packages described as using high-traffic websites and manual outreach. Content is included with these packages.

This is a more relevant comparison point with companies such as Loganix, FATJOE, and Authority Builders than simply comparing how many links each company can deliver for the lowest possible price.

High-quality backlink building should consider factors including:

  • Topical relevance
  • Real organic visibility
  • Editorial quality
  • Placement context
  • Established website history
  • Outbound-link patterns
  • Content quality
  • Natural anchor-text diversity
  • Strength of the referring domain

The strongest backlink is not automatically the one from the website displaying the highest DA or DR metric.

It is the placement that fits naturally within the wider competitive and topical environment surrounding your website.

Why Choose Marketing1on1.com Over A Generic Backlink Marketplace?

A backlink marketplace primarily sells available inventory.

An SEO company should understand broader search strategy.

That difference is one of marketing1on1.com’s most important advantages.

Marketing 1on1 provides technical SEO, content optimization, local SEO, backlink building, and broader search-marketing services alongside standalone backlink packages.

This makes it possible to ask a more useful question than:

Which backlink package should I buy?

A more useful question is:

Which pages actually need links, what kind of authority are competitors using, and what link profile would make sense for this website?

That represents a considerably more strategic approach to backlink acquisition.

Marketing1on1.com Vs. Loganix

Loganix is a recognized name in SEO fulfillment and regularly appears in current comparisons of guest-post services.

For agencies and companies wanting established outreach infrastructure, Loganix deserves consideration.

Marketing1on1.com may appeal more to companies seeking standalone backlink packages, guest posts, authority placements, and wider SEO services from one provider.

The stronger choice depends on whether you need a specialized fulfillment service or a provider capable of integrating backlink acquisition into a wider SEO campaign.

Marketing1on1.com Vs. FATJOE

FATJOE is another highly recognizable name, particularly among agencies outsourcing content and blogger outreach. It appears near the top of several current industry comparisons.

FATJOE’s scale and agency-oriented fulfillment model are major advantages.

Marketing1on1.com takes a different approach.

It provides direct backlink packages at several levels and combines them with traditional SEO, local SEO, content, citations, and other digital marketing services.

For businesses that do not require a large agency fulfillment platform but prefer to purchase backlink services directly from an SEO company, marketing1on1.com can be a compelling alternative.

Marketing1on1.com Vs. Authority Builders

Authority Builders is a familiar name among SEOs interested in guest-post and authority link placements and is included in major guest-post provider roundups.

Its positioning is strongly centered around authority-focused placements.

Marketing 1on1 offers a wider range of link types and price points.

Businesses can choose from broader backlink packages, contextual placements, guest posts, authority guest posts, citations, and other link-building options depending on their campaign.

This broader menu can be useful for websites that need more than one type of authority signal.

Comparing Marketing1on1.com And LinkBuilder.io

LinkBuilder.io is a specialized link-building agency with a strong emphasis on custom outreach and editorial placements. Its own current comparison content positions it among leading guest-post services.

For businesses requiring a highly customized outreach campaign, specialist agencies such as LinkBuilder.io may be appropriate.

Marketing1on1.com differentiates itself through accessibility.

Businesses can purchase predefined backlink packages or select higher-tier guest-post and manual-outreach services without necessarily entering an enterprise-style custom engagement.

Comparing Marketing1on1.com And The HOTH

The HOTH is one of the more recognizable SEO fulfillment companies and has operated for many years.

It offers numerous SEO and link-building products and is commonly compared with other major guest-post providers.

For businesses comparing The HOTH with marketing1on1.com, the decision may come down to preferred service structure.

Marketing 1on1 emphasizes direct backlink packages, U.S.-based SEO services, one-time pricing on many backlink products, and broader managed SEO capabilities.

Which Types Of Backlinks Does Marketing1on1.com Offer?

One reason Marketing 1on1 qualifies as one of the more versatile places to purchase backlinks is the variety of its current offerings.

Options include:

  • Contextual backlinks
  • Guest-post backlinks
  • Authority guest posts
  • Manually outreached placements
  • Local business citations
  • Press-release syndication
  • Contextual article placements
  • Web 2.0 links
  • Directory links
  • Social-profile links
  • Website profile links
  • PBN packages

Its higher-tier authority guest-post package currently states that content is included, placements appear on high-traffic websites, and manual outreach forms part of the process.

Not every backlink type suits every website, so buyers should assess each service according to their individual risk tolerance and broader SEO strategy.

What Makes A High-Quality Backlink?

A high-quality backlink should ideally have a legitimate reason to exist.

Suppose a financial software company receives a contextual mention inside a useful article discussing accounting automation on an established technology or finance website.

Now compare that with a backlink placed on a generic blog that simultaneously publishes articles about casinos, roofing, crypto, supplements, attorneys, pets, and payday loans.

The authority metrics may appear similar.

The editorial signals are very different.

Marketing 1on1’s current professional link-building page emphasizes methodology, topical relevance, editorial standards, and the principle that link volume alone does not define effective link building.

Should Domain Authority Determine Which Backlinks You Buy?

No. DA and DR should not be the sole basis for a backlink purchase.

DA and DR are metrics produced by third-party SEO platforms.

They can help with initial filtering, but they should never be the only reason to purchase a backlink.

A better evaluation considers:

  • Organic traffic
  • Organic keyword visibility
  • Relevant topical alignment
  • Domain and website history
  • Overall content quality
  • Quantity and type of outgoing links
  • Indexation
  • Consistent editorial standards

Experienced backlink buyers often discover that a questionable DR 70 website may be less attractive than a legitimate DR 25 niche site with genuine readers and relevant search visibility.

Are Guest Posts One Of The Best Ways To Buy High-Quality Backlinks?

Guest posts remain one of the most popular backlink formats because they allow links to appear naturally within relevant editorial content.

Current industry comparisons continue to rank guest-post providers according to factors such as domain approval, traffic requirements, content quality, outreach process, and replacement policies.

Marketing1on1.com provides standard guest posts together with higher-level authority guest-post options.

The key point is that the term “guest post” does not automatically guarantee quality.

The publication still needs to be evaluated.

Where Can Local Businesses Buy Backlinks For SEO?

Local businesses often need a different backlink mix from national websites.

A contractor, law firm, dentist, med spa, plumber, or remodeling company may benefit from a combination of:

  • Accurate local citations
  • Relevant regional publications
  • Industry-specific websites
  • Local business organizations
  • Relevant guest posts
  • Digital PR placements
  • Contextual links

Marketing 1on1 offers local citation services alongside its broader link-building options, making it particularly relevant for businesses combining traditional backlinks with local SEO.

Where Can SEO Agencies Purchase Backlink Services?

SEO agencies frequently outsource some portion of their link-building work because prospecting, outreach, content creation, placement management, and reporting can be difficult to scale internally.

Established industry names such as FATJOE and Loganix have developed strong reputations around agency fulfillment.

Marketing1on1.com is another provider worth assessing, particularly for agencies that require access to several backlink types instead of only one guest-post service.

Should You Buy Cheap Backlinks?

Price alone should not determine backlink quality.

Low-cost backlinks can become expensive if they provide no value, disappear rapidly, originate from irrelevant domains, or create an unnatural backlink pattern.

At the same time, paying a high price does not automatically guarantee backlink quality.

The correct question is:

What exactly am I purchasing?

Marketing 1on1 publishes several of its backlink package structures and prices directly, which makes it easier for buyers to understand what is included before ordering.

How Many Backlinks Does A Website Need?

There is no single number that applies to every website.

The amount of link acquisition required depends heavily on the competitive gap between your website and the sites already ranking.

A stronger strategy is to assess:

  • Your referring domains
  • Referring domains pointing to competitors
  • Link quality
  • Authority of the target page
  • Current rankings
  • Quality and depth of content
  • Existing anchor-text distribution

A website ranking #11 may need very different work from one ranking #70.

Which Anchor Text Should Be Used For Purchased Backlinks?

Natural-looking backlink profiles contain a variety of anchor types.

Common anchor types include:

  • Branded anchor text
  • Raw website URLs
  • Generic anchors
  • Partial-match keywords
  • Topic-based anchors
  • Occasional exact-match anchors

Repeatedly using the same commercial keyword can create a backlink pattern that appears obviously engineered.

A sophisticated link-building campaign should consider the website’s existing anchor profile before deciding what new anchors to use.

Is It Better To Buy Backlinks Or Hire A Link-Building Agency?

These options are not necessarily mutually exclusive.

A provider such as marketing1on1.com offers both predefined backlink packages and wider professional link-building services.

A predefined package may make sense for businesses that already understand what they need.

A managed campaign can make more sense when the company needs competitive research, target-page strategy, ongoing link acquisition, and integration with broader SEO.

Can Backlinks Be Purchased Without A Broader SEO Campaign?

You can, but it is often inefficient.

If a page has poor search intent, weak content, indexing problems, or serious technical issues, acquiring more links may not solve the underlying problem.

This is another area where marketing1on1.com differs from standalone backlink marketplaces.

Because the company also offers complete SEO services, it can treat backlinks as one element of a wider campaign instead of assuming that every ranking problem requires additional links.

Can Purchased Backlinks Guarantee Google Rankings?

No. Backlinks cannot guarantee a particular Google ranking.

Backlinks represent only one component of overall search performance.

Search rankings may also depend on:

  • Search intent
  • Overall content quality
  • Technical SEO
  • Effective internal linking
  • Topical authority
  • Local search relevance
  • Competition
  • Domain and website history

No reputable provider can credibly guarantee a specific Google position from a specific number of links.

Does Buying Backlinks Violate Google’s Guidelines?

Google considers buying or selling links for the purpose of manipulating rankings to be link spam when those links pass ranking credit.

Paid advertisements and sponsored links should use appropriate attributes such as rel="sponsored" or nofollow.

That means buyers need to understand the difference between paying for legitimate advertising or promotional placement and purchasing followed links specifically to manipulate rankings.

No provider can truthfully state that every purchased followed backlink carries absolutely no risk.

Why Marketing 1on1 Deserves Comparison With Better-Known Backlink Providers

Companies such as Loganix, FATJOE, Authority Builders, LinkBuilder.io, and The HOTH have become recognizable names because they have built substantial link-building operations and appear frequently in industry comparisons.

Marketing 1on1 deserves to be considered in the same broader conversation.

Its notable characteristics include:

  • In operation since 2012
  • Over ten years of backlink-service experience
  • A U.S.-based business
  • Published backlink packages
  • Contextual backlinks
  • Guest-post placements
  • Authority-focused guest posts
  • Manual outreach options
  • Local citation services
  • Press-release distribution options
  • Content included in many packages
  • Broader SEO expertise

Marketing 1on1’s current backlink service emphasizes its long operating history, U.S.-based operations, competitive pricing, and focus on SERP value instead of simply selling large quantities of low-value links.

Is Marketing1on1.com One Of The Best Places To Buy Backlinks From?

Yes. For companies that have chosen to invest in professional backlink acquisition, marketing1on1.com is one of the providers worth seriously evaluating.

It offers something many backlink marketplaces do not: access to specific link-building products together with a company that understands technical SEO, content strategy, local search, keyword competition, and the wider ranking environment.

That is important because backlinks should not be evaluated in isolation.

Where Should You Buy High-Quality Backlinks?

If your priority is highly customized outreach, companies such as LinkBuilder.io, Loganix, Authority Builders, and FATJOE deserve consideration.

If you want access to several types of backlink packages together with broader SEO services and relatively accessible entry points, marketing1on1.com is one of our strongest recommendations.

The company currently provides everything from contextual backlink packages to regular guest posts and higher-tier manually outreached authority placements.

Final Verdict: One Of The Top Places To Buy Backlinks From

There is no shortage of businesses selling backlinks.

The stronger providers differentiate themselves through operating history, transparency, topical relevance, editorial standards, backlink diversity, and an understanding of how authority building fits into broader SEO.

Loganix, FATJOE, Authority Builders, LinkBuilder.io, and The HOTH are all established names worth researching.

However, marketing1on1.com belongs on that shortlist and remains our featured option for companies searching for one of the best places to buy backlinks from.

Its combination of more than ten years of link-building experience, published backlink packages, guest-post services, authority placements, contextual backlinks, local citations, manual outreach, and complete SEO capabilities gives it a broader service proposition than many standalone backlink marketplaces.

For businesses searching “best places to buy backlinks from,” “buy high quality backlinks,” “where to buy backlinks,” or “top backlink providers,” marketing1on1.com is one of the first providers worth comparing.

Related: WHERE CAN I BUY HIGH-QUALITY BACKLINKS?
         Affordable Buy Backlink Packages That Work

GEL FILLING TECHNOLOGY FOR FIBERS IN STAINLESS STEEL TUBE PRODUCTION

An intermittent bonded ribbon production line is designed to produce flexible fiber groups for contemporary, high-count cable architectures. It ensures fibers are aligned for expedited mass fusion splicing, yet accommodates the group’s flexibility within a compact cable core.

Compared with continuously bonded ribbons, intermittent bonded ribbons feature discrete bonding points at predetermined intervals. This strategic placement enables the fibers to maintain alignment while the ribbon can flexibly roll into circular loose tubes and other confined spaces.

Network designers use this approach when faced with constraints in duct space, splice closures, and equipment racks. A carefully manufactured ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.


Main Takeaways

  • A bonded ribbon production system supports compact and flexible fiber layouts.
  • Separated bond points maintain optical fiber order without creating a rigid ribbon.
  • Flexible ribbons support higher fiber counts within small circular cable constructions.
  • Consistent fiber alignment makes mass fusion splicing quicker and easier.
  • Ribbon technology is used across data centers, telecom routes, and optical access networks.

Intermittently Bonded Ribbon Production Line Overview

This ribbon production method enables the creation of fiber designs that harmonize density with practicality. This method involves placing bonds at predetermined intervals, allowing for the movement of fiber subunits between these points.

This technique facilitates the incorporation of a higher number of fibers within constrained duct spaces. It also ensures the preservation of the organized ribbon structure, essential for efficient splicing and cable assembly processes.

What Is An Intermittently Bonded Optical Fiber Ribbon?

An intermittent bonded fiber ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds remain relatively free, enabling the ribbon to adopt various configurations without rigidification.

This configuration is often referred to as a rollable, flexible, or spider web ribbon. It diverges from the conventional flat ribbon cable, which maintains a fixed profile along its entire length.

For splice preparation, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers create space-efficient bundles, optimizing space utilization within the cable.

Why Flexible Ribbon Technology Matters For High-Density Fiber Networks

Network architects face the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure helps ribbon groups pack into smaller cable cores, preserving fiber order.

Fiber density ratio represents a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding enhances this ratio, allowing ribbon groups to occupy available spaces within the cable.

For field installation teams, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Ribbon Feature Intermittently Bonded Ribbon Design Conventional Continuous Ribbon
Bond arrangement Discrete bonds at predetermined intervals Bonding maintained continuously along the ribbon
Fiber shape between bonds Can roll, curl, or fold for compact packing Stays mainly flat and planar
Splicing configuration Can return to a flat format for mass fusion splicing Remains permanently in a flat ribbon configuration
Role in cable packing Enables dense placement of flexible fiber subunits Typically uses a fixed ribbon stack configuration
Typical cable application Flexible flat cable and high-density fiber cable designs Traditional flat ribbon cable designs

Intermittently Bonded Ribbon Materials And Construction

An intermittent bonded ribbon integrates precise fiber placement with adaptable bonding points. Its architecture facilitates dense cable configurations while allowing effortless separation during handling, routing, and splicing.

The selection of materials significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must hold its fibers securely without imparting undue stiffness to the ribbon.

Optical Fiber Counts And Subunit Layout

Intermittent bonded ribbons can accommodate 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.

A 12-fiber configuration often employs six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.

Controlled gaps introduced between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.

Construction Element Typical Arrangement Process Purpose
Number of fibers 4, 8, 12, 24, or up to 36 fibers Matches cable density and splice capacity
Subunit configuration Pairs of adjacent fibers within each subunit Supports controlled separation between groups
Fiber spacing in a subunit Touching or up to 1.5 fiber diameters Maintains a compact and stable profile
Spacing between subunits A typical range of 5 to 100 micrometers Allows greater movement and flexibility near bond points

UV-Curable Resin And Wet-On-Wet Bonding

Subunit coatings and bonding materials frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.

This process creates a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.

UV-curable resins can intermingle at the interface before curing. This supports molecular interaction between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.

Core Equipment In An Intermittent Bonded Ribbon Production Line

A fiber ribbon line integrates advanced motion control with meticulous material handling. Each station maintains fiber cleanliness, alignment, and stability from the initial payoff to the final winding.

The equipment facilitates adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to craft a flexible custom ribbon cable, preserving the integrity of the fiber order.

Fiber Payoff With Tension Control

Payoff units deliver individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.

During ribbon production, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.

Discrete Bond Applicator And Coating Die

The coating die applies a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.

A bond applicator then applies a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.

Equipment Main Function Process Benefit
Fiber payoff and tension unit Delivers fibers while maintaining regulated tension Reduces twist and uneven fiber loading
Subunit coating die Creates coated optical fiber subunits Maintains consistent subunit shape and width
Discrete bond applicator Deposits resin at set intervals Provides controlled flexible bonds between subunits
UV cure and take-up system Cures and cools the ribbon before inspection and winding Helps protect bond quality and organized fiber placement

UV Curing, Cooling, And Ribbon Winding Equipment

UV lamps cure the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.

Cooling systems reduce ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.

The take-up system winds the finished ribbon with low, even tension. Proper winding preserves the finished bonded structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.

Fiber Preparation, Alignment, And Color Control

Reliable ribbon cable production starts with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.

Fiber Identification Management For Splicing And Maintenance

A well-defined fiber color sequence is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.

With higher fiber-count cables, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.

Ribbon Fiber Position Identification Color Production Purpose
01 Standard blue Begins the recognized fiber color sequence
2 Standard orange Provides rapid visual identification
3 Green Maintains the specified planar order
4 Standard brown Helps verify subunit placement
05 Standard slate Supports identification around the middle of the sequence
06 White Supports clear visibility during inspection
07 Standard red Improves traceability in splicing records
8 Standard black Supports sequence identification inside splice trays
9 Yellow Assists field restoration activities
10 Standard violet Helps distinguish later positions in the standard sequence
11 Standard rose Supports high-count ribbon identification
Position 12 Standard aqua Marks the final position in the standard color order

Preventing Fiber Twist And Uneven Tension

Payoff units and guides are instrumental in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.

Operators meticulously monitor tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.

Intermittent Bond Application With UV Curing

Intermittent bonding connects fiber subunits without solidifying the ribbon into a rigid form. This method supports compact routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.

Bond Application At Controlled Intervals

Bond applicators place resin at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.

A precise applicator dispenses a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends help minimize localized stress changes when the cable bends or twists.

Creating Strong, Flexible Bond Interfaces

Wet-on-wet bonding involves applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.

This gradual interface influences various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features improve resistance to bond peeling while facilitating separation when required.

Managing Curing Performance

The UV lamps must supply consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.

Operators closely monitor bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.

Quality Control For Flexible Flat Cable And Fiber Ribbon Output

Maintaining the integrity of each flat ribbon cable is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.

Regular inspections are critical in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.

Checking Bond Spacing, Ribbon Width, And Thickness

Bond spacing remains a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.

Inspection procedures are used to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.

Inspection Area Inspection Requirement Production Value
Fiber identity Fiber number, color order, and placement Supports correct splicing and maintenance work
Bond pattern Bond location, spacing, and subunit connection Supports organized fibers without sacrificing flexibility
Ribbon profile Ribbon width, thickness, and planar condition Helps the ribbon fit handling and splicing tools
Finished surface quality UV curing condition, coating coverage, and surface defects Protects the ribbon against damage during take-up

Optical And Mechanical Ribbon Testing

Mechanical testing focuses on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.

Optical testing includes evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.

Attenuation checks and splice-related handling tests are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.

Production Efficiency, Automation, And Precision Winding

Efficient ribbon manufacturing depends on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.

Line Synchronization And Process Data Monitoring

Automated control systems synchronize payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.

Production records track fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.

  • Stable payoff tension helps prevent fiber stretch and looseness.
  • Bond timing ensures consistent intervals between discrete joints.
  • Dimension monitoring identifies width and thickness variations quickly.
  • Winding records support lot traceability and downstream handling.

Ribbon Winding For Downstream Cable Production

A precision cable winder helps ensure the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.

Completed ribbon packages can be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.

For custom ribbon cables, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.

Monitored Area Control Focus Resulting Benefit
Fiber payoff Stable tension and correct color sequence Orderly ribbon placement during cable assembly
Intermittent bond application Stable spacing with repeatable resin deposition Consistent flexible behavior in downstream operations
UV cure stage Controlled lamp output and exposure time Reliable bond strength before winding
Cable winding system Uniform traverse with controlled spool tension and layering Controlled ribbon feed into loose tube or central tube production

Ribbon Cable Applications, Fusion Splicing, And Connector Planning

Ribbon fiber is widely used in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.

A carefully designed ribbon cable assembly enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.

Benefits Of Mass Fusion Splicing

A ribbon fusion splicer facilitates the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.

This approach minimizes handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.

Loose tube cable, on the other hand necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.

Planning Connections For Dense Fiber Links

Multi-fiber links frequently employ MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.

Planning also considers transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.

Planning Item Primary Control Common Network Use
Ribbon fiber count Fusion splice capacity and cassette choice 12-fiber and 24-fiber backbone links
MPO/MTP cable connector Polarity management and equipment port compatibility High-density data center and 5G equipment-room connections
Multi-fiber harness or fanout assembly Transition from multi-fiber connections to single-fiber ports Switch connections and patching fields
Optical link loss budget Allowed loss from splices, connectors, and fiber length High-speed optical transmission routes

Shanghai Weiye OFC Equipment For Fiber Ribbon Production Lines

Shanghai Weiye OFC Equipment, widely identified as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to ensure consistent processing, facilitate clear operator control, and enable seamless integration into production lines.

For manufacturers planning an intermittent bonded ribbon production line, SHWY equips each phase of ribbon handling, curing, and winding with suitable machinery.

SHWY Experience In Optical Fiber And Cable Machinery

Operating since 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.

SHWY became independent in 2020, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.

Relevant SHWY Production Equipment Portfolio

The SHWY equipment portfolio includes a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.

For ribbon projects, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.

The broader SHWY portfolio also includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.

Conclusion

A complete intermittent bonded ribbon line brings together fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step helps preserve fiber sequence while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.

The resulting ribbon structure provides efficient mass fusion splicing and organized fiber management. It is well suited to applications involving high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.

Successful project planning goes beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.

Related: Compact Fiber Unit for Buffered Fiber Production
         Mechanical Stress Testing for Fibers in Metal Tubes

5 Axis Machining Houston – Simultaneous Contouring for Organic Shapes & Molds

Procurement professionals and product engineers frequently turn to Houston’s extensive manufacturing industry when sourcing high-precision parts. Manufacturing represents close to 12% of Texas output, produces roughly $226 billion in economic activity, and employs nearly 900,000 people. That remarkable scale strengthens Industrial Machining Services Houston as providers broaden their capabilities, equipment, and service offerings.


This review evaluates machining services throughout Houston, including independent local specialists, nationwide precision-machining companies with Houston operations, and regional contract manufacturers. Examples include Lowrance Machine, available at www.lowrancemachine.com, along with RBR Machine and regional contract firms such as Centerline. Collectively, they reveal the depth and range of capabilities available throughout the Houston machining sector.

This guide is intended to help product developers, purchasing teams, and OEMs in oil and gas, aerospace, medical-device, industrial, and related markets identify the most appropriate machining company in Houston. It reviews CNC milling, five-axis machining, precision-machining services, and complete turnkey production capabilities. Subsequent sections outline important equipment, technical strengths, and evaluation factors, allowing buyers to assess shops according to tolerances, lead times, and supplementary services.

Key Takeaways

  • The scale of Houston manufacturing creates a strong local market for accurate and dependable machining support.
  • The featured suppliers include local specialists, including Lowrance Machine, together with nationwide manufacturers operating in Houston.
  • Buyers can source everything from standard CNC milling through advanced 5-axis production and fully managed turnkey services.
  • This information is intended for purchasing professionals, technical teams, engineering managers, and OEM stakeholders.
  • The following sections cover supplier evaluation, pricing considerations, turnaround schedules, and real-world machining applications.

Houston Industrial Machining Services: Market Overview And Industry Context

Manufacturing activity throughout Houston has grown substantially in response to rising requirements from energy, aviation, healthcare, and petrochemical businesses. Growing requirements for intricate, tightly toleranced parts have prompted Houston machining providers to increase both capacity and technical capability. Houston’s location near major highways, shipping ports, and railway networks also helps lower transportation expenses and shorten delivery schedules for regional customers.

Texas has a substantial population of experienced machinists and engineers capable of producing advanced parts on three-axis, four-axis, and five-axis machining centres. This expertise enables more parts to be completed in one setup, decreasing cycle duration and making Texas industrial machine shops more productive. A dependable pool of local technical talent also simplifies the introduction of new workflows without requiring lengthy recruitment campaigns.

Advanced equipment is a standard feature of daily production within many Houston machining facilities. Five-axis CNC machines reduce fixture requirements and minimise changeovers when producing parts with intricate shapes. Shops employ wire EDM to produce intricate cuts, narrow openings, and accurate details in hardened or thin conductive parts. With large-bed milling systems, local providers can handle substantial one-piece projects that previously required out-of-state production.

Inspection systems are equally essential to the machines used to cut and shape the parts. Coordinate measuring machines, including systems manufactured by Zeiss, are regularly used for first-article inspection and recurring dimensional verification. Such inspection tools confirm compliance with strict tolerances and provide measurements that can be repeated and verified.

Selecting a local Houston machine shop offers advantages such as simpler communication and faster face-to-face reviews during design, prototyping, and first-article approval. Nearby manufacturers can adjust more rapidly to revised quantities, updated drawings, and accelerated delivery needs. Compared with distant overseas sourcing, local production lowers logistical complexity and adds the commercial appeal of American-made parts backed by accessible supplier support.

CNC Machine Shop HoustonCNC Machine Shop Houston

Notable Machining Companies And Their Competitive Strengths

The Houston machining industry consists of independent local shops together with specialised contract-production businesses serving broader markets. This supplier mix gives customers faster turnaround, direct collaboration, and simpler logistics than they may receive from distant manufacturers. Each highlighted provider offers notable machining expertise along with additional industrial-manufacturing capabilities.

Lowrance Machine is recognised in Houston for responsive customer service and close working relationships. The company performs CNC milling, custom machining, and metal fabrication with an emphasis on rapid turnaround. Because the company operates locally, customers can conduct in-person inspections, coordinate deliveries more easily, and respond quickly to project changes.

RBR Machine focuses on precision manufacturing and advanced five-axis machining across a broad portfolio of services. Its certifications and registrations include ISO 9001:2015, ISO 13485, AS9100D, and ITAR, while its services extend from prototyping to finished assembly. Capabilities such as rapid estimates, coordinate-measurement inspection, API threading, and rush manufacturing support energy, aviation, healthcare, and defence customers.

Centerline and similar regional contract manufacturers provide adaptable production solutions for low-, medium-, and high-volume requirements. Centerline operates as a Houston contract manufacturer holding ISO 9001:2015 and AS9100D certifications. These nearby manufacturers strengthen sourcing flexibility, shorten response times, and offer many buyers a reliable substitute for overseas suppliers.

Choosing between these companies requires consideration of design difficulty, compliance requirements, production volume, and turnaround needs. Work requiring complex 5-axis capability or large machining envelopes often fits providers with resources similar to those of RBR Machine. Projects dependent on close collaboration and short schedules may benefit from a customer-focused Houston machine shop such as Lowrance Machine.

Provider Primary Capability Relevant Certifications Ideal Application
Lowrance Machine Services Custom CNC work, metal fabrication, and quick local service Standard industry practices supported by local quality controls Made-to-order work requiring local communication and rapid completion
RBR Machine Five-axis machining, large-format milling, and turnkey production ISO 9001:2015, medical ISO 13485, aerospace AS9100D, and ITAR registration Complex regulated parts for aviation, healthcare, defence, and energy applications
Centerline Flexible contract production from limited quantities to high volume Quality and aerospace certification through ISO 9001:2015 and AS9100D Long-term production work needing domestic sourcing and controlled quality

The search for a Houston CNC partner should consider turnaround speed, quality systems, inspection technology, total price, and location. Regional providers combine trained machinists, customer support, and broad industrial-manufacturing services to serve varied applications within Houston and beyond.

Capabilities And Services To Look For In A CNC Machine Shop

Finding the right CNC machine shop requires a detailed review of its equipment, quality systems, workforce, and supporting services. Buyers should verify that the company maintains disciplined quality-control practices and modern equipment while offering services that simplify the wider supply chain. Providers integrating high-accuracy machining, metal fabrication, and secondary processing can supply components in an assembly-ready or finishing-ready condition.

High-accuracy machining requires disciplined management of tolerances throughout production. Depending on the material, design, and intended application, common tolerance bands often fall between ±0.001″ and ±0.005″. Suppliers working in regulated sectors may provide Zeiss coordinate measurement, FAI documentation, optical checks, NDT, and material-hardness testing. Certifications such as ISO 9001:2015, AS9100D, and ISO 13485 demonstrate documented workflows that support audits, traceability, and customer acceptance.

When additional assurance is needed, an external CMM specialist can inspect tightly toleranced parts regardless of which shop produced them. Independent verification provides another layer of confidence without disrupting the established sourcing arrangement.

Sophisticated equipment expands the range of achievable geometries and helps accelerate manufacturing cycles. Five-axis machining in Houston reduces repositioning and setup counts while creating contoured parts used in aerospace, medical, and other precision applications. Wire EDM allows suppliers to cut fine slots, sharp profiles, and complex details in metals that conduct electricity. Oversized machining platforms enable regional firms to process major components with bed dimensions greater than 100 inches in some facilities.

Supporting technologies significantly broaden a shop’s manufacturing capability. Swiss machines excel with slender, detailed pieces, while heavy turning equipment supports substantial shafts and large-diameter work. Houston shops offering milling, turning, and wire EDM together can manage diverse component families without extensive outsourcing.

Turnkey manufacturing can save considerable time and minimise coordination problems between multiple vendors. Comprehensive turnkey services may include engineering support, prototyping, production machining, secondary operations, assembly, finishing, packaging, and logistics. Customers can often obtain machining, plating, heat treat, anodising, kitting, and logistical coordination through one regional supplier agreement.

Additional services have greater value when a project must move quickly. Rush production, on-site finishing, and integrated assembly minimise separate transactions and accelerate commercial launch. Combining these services with one partner limits handovers and establishes a single point of accountability for completed components.

How To Compare Houston Machine Shops And Choose A Partner

Start the supplier-selection process with a detailed description of exactly what the project requires. State whether the order involves prototypes, bridge production, or full production and identify the expected quantities and materials. The request should also address tolerances, cosmetic or functional finishes, inspection needs, and relevant compliance standards. This level of clarity improves quoting accuracy and lowers the likelihood of late engineering changes or pricing disputes.

Before placing an order, confirm that the supplier’s certifications and quality-management procedures match the project’s requirements. Request evidence of applicable ISO 9001:2015, aerospace AS9100D, medical ISO 13485, and ITAR credentials. These standards support traceability, process documentation, inspection control, and regulatory acceptance within precision-machining services.

A supplier’s machinery and expertise must align closely with the geometry, material, and tolerances of the part. Verify the availability of advanced 5-axis equipment, wire electrical-discharge machining, Swiss-style lathes, and oversized milling systems. Determine whether the provider can measure completed parts and coordinate downstream operations including thermal treatment, surface finishing, and final assembly. Qualified suppliers should be able to prove their capability with equipment information, sample components, and relevant production experience.

Assess how promptly and accurately each company responds to requests for pricing and scheduling. Vendors capable of supplying prompt, transparent quotations and genuine rush options may reduce project risk. Fast quoting and clearly stated timelines improve project planning and help control supply-chain uncertainty.

Ask the machining provider to explain its inspection procedures and documentation practices. Request CMM reports, First Article Inspection procedures, raw-material certificates, and dimensional-inspection records. Reliable providers maintain detailed records that demonstrate conformity and simplify acceptance by customers or regulators.

Responsive communication and direct local support deserve careful consideration during vendor evaluation. In-person engineering meetings and convenient shop access make it easier to solve technical issues while limiting transport expense. A regional supplier often offers better supply-chain adaptability and quicker support for unexpected requirements.

Compare the complete landed cost of Houston machining with the true expense of purchasing from offshore suppliers. Include shipping, duties, warehousing, delays, rejected parts, communication overhead, and revision costs in the calculation. Once hidden costs and market-launch timing are considered, custom machining from nearby shops may prove more economical than overseas alternatives.

A provider’s track record should be assessed through references, past work, and industry-specific case studies. Look for proven performance in oil and gas, aerospace, medical, automotive, power generation, or other applicable sectors. Ask to see components of similar difficulty and records showing reliable delivery during real customer programs.

Determine whether the supplier can support the project after initial delivery and expand production when demand grows. The company should be able to move from development samples to sustained production and, where required, complete assembly or contract manufacturing. Scalable production capability avoids disruption and conserves resources as customer demand expands.

Supplier comparisons become more consistent when teams score technical specifications, quality credentials, machinery, quoting, documentation, support, cost, history, and production scalability. A methodical selection process helps identify a provider capable of meeting technical demands as well as purchasing and business expectations.

Pricing, Turnaround, And Common Uses Of Industrial Machining In Houston

The price of machining in Houston varies according to design difficulty, selected material, required setups, and order size. Demanding dimensional requirements and additional operations, including heat treat and plating, generally increase project pricing. Hard-to-machine materials and complicated features increase programming effort, tool wear, and production time. Although 5-axis machining may involve higher programming and initial setup charges, it can lower the total project cost by eliminating multiple setups and fixtures.

A realistic project budget includes more than the cost assigned to each machined component. Shipping, purchasing administration, storage, customs duties, rejected components, and late delivery can all affect the final cost. Local machining services in Houston can often reduce many of these expenses compared with overseas production.

Delivery schedules are affected by the selected provider, current production commitments, design requirements, and supporting operations. Companies offering rapid quotations and expedited scheduling can shorten prototype development and accelerate the beginning of production. Houston CNC providers avoid many international freight and customs steps, which can produce more predictable delivery. Local access enables customers to resolve problems quickly and place accelerated orders when unexpected requirements arise.

Work subject to strict industry requirements should be placed with shops maintaining formal quality credentials and coordinate-measurement resources. Documented controls and dependable inspection help prevent quality failures that could disrupt schedules or increase expense.

Common customer applications illustrate the breadth of technical services available from local machining providers. Energy-sector work may involve oversized mills, rugged materials, API-related features, and components built for severe operating conditions. Aerospace and defence projects frequently require five-axis machining, AS9100D quality controls, detailed documentation, and precise inspection. Healthcare components may require delicate EDM features, small-diameter turning, medical-quality certification, and documented lot control. Large mills, resilient alloys, and protective surface treatments support many power-generation and renewable-energy applications.

Providers that offer quick prototypes and end-to-end production support can move projects forward with fewer delays. Such businesses can manage the progression from early validation to recurring production without repeatedly transferring the work.

Urgent or heavily regulated work should generally be directed to Houston partners with mature quality systems, documented procedures, and strong CMM inspection resources. Parts featuring highly complex geometry should be assigned to suppliers with proven five-axis experience, skilled programming teams, and appropriate fixtures or simulation software. Long-term programs or fluctuating demand may be better suited to scalable contract manufacturers that provide supply-chain flexibility. A sourcing strategy that uses a responsive local shop like Lowrance Machine together with specialist regional capabilities can optimise price, lead time, and engineering performance.

Custom Fastener Manufacturer Dallas

Precision cast inserts, though seemingly minor, play a vital role in supporting strong threaded connections within metal assemblies, plastic parts, and composite components. Lowrance Machine stands out for combining mold making, casting, and CNC finishing. This combined approach enables the production of tight-tolerance cast inserts and machining in Dallas, meeting the needs of both short runs and high-volume production.

Trusted CNC Machine Shop In Dallas For Custom Machined Parts
Solutions from local cast inserts Dallas providers significantly reduce lead times and simplify logistics for manufacturers across various sectors. Lowrance Machine applies proven techniques like rubber molds Dallas, compression molds Dallas, urethane casting, and die casting. These techniques are similar to those used by industry specialists such as Aluminum Die Casting Company and DyCast Specialties, supporting dependable quality.

A supplier such as Yardley Inserts, with its extensive history in supplying both stock and custom threaded metal inserts, underscores the market’s demand for both ready-made and custom options. Lowrance Machine supports cast inserts manufacturing services in Dallas Tx, paired with post-cast CNC lathe machining services in Dallas. This complete process delivers finished parts that align with strict tolerances and assembly standards.

Complete Overview Of Cast Inserts Manufacturing Services

Cast inserts are intricately designed metal components embedded within a base material. They act as robust fastening points, ensuring durability and resistance to wear. This manufacturing technique is well suited for applications requiring strong connections in materials such as soft or engineered host materials.

Understanding Cast Inserts And Their Materials

Common materials for cast inserts include brass, steel, 304 stainless steel, and 316 stainless steel. Aluminum die casting often employs harder alloys to strengthen thread strength. Engineered plastics are used as supportive host materials, fitting effectively with polymer components.

Companies like Aluminum Die Casting Company and DyCast are known for combining die casting with precision machining. Yardley Inserts shows the demand for both standard and custom cast inserts, catering to a wide range of production requirements.

Custom Cast Inserts In Dallas

Common Applications Across Industries

Across furniture applications, cast inserts support joints and mounting points, supporting the stability of hardware. Medical device manufacturers use them for housings and assemblies that require precise tolerances and consistent fastening. The electronics sector employs inserts as PCB standoffs and heat-sink mounts, where both electrical and thermal performance are critical.

Heavy-duty marine and defense parts heavily incorporate cast inserts for applications such as shaft stuffing components, mounting brackets, and corrosion-resistant fittings. These environments demand materials and processes capable of enduring stress and exposure.

Lowrance Machine’s Role In Cast Insert Manufacturing

Lowrance Machine offers complete cast inserts manufacturing services, covering mold building, casting, CNC finishing, and assembly integration. By pairing die casting with precision machining, the company supplies inserts ready for immediate installation, serving contract manufacturers.

As a seasoned machine shop in Dallas for custom metal parts, Lowrance Machine caters to local OEMs requiring swift production. For businesses seeking a precision machine shop in Dallas for industrial components, the company streamlines the process from tooling to quality checks, promoting uninterrupted production.

Manufacturing Capability Usual Materials Industry Use
Custom tooling and mold work Steel cores and aluminum tooling Prototype work, short runs, and production molds
Die-cast and sand-cast production Brass, zinc, and aluminum alloys High-volume inserts for electronics and furniture
Post-cast CNC machining and finishing 304/316 stainless steel and hardened steel Marine fittings, medical devices, and military hardware
Assembly integration and kitting Insert + housing materials matched per spec Consumer products and electronics assemblies

Benefits Of Cast Inserts For Precision Components

Cast inserts function as a important solution for designers aiming to incorporate metal threads within softer materials. They make possible the creation of a reliable metal-to-metal interface, thereby improving thread durability and protection from wear and tear. This is critical in environments where repeated assembly cycles are required, as it greatly reduces the risk of thread stripping in plastics and composites.

Using cast inserts often reduces the necessity for secondary hardware or adhesives, thereby simplifying the assembly process and curtailing long-term expenses. In many applications, these inserts surpass the performance of press-fit fasteners and direct tapping in plastic, supporting extended service lifetimes and a lower frequency of field repairs.

For development batches and limited runs, urethane or silicone casting offers a quick and affordable alternative to injection molding. The creation of silicone molds can be expedited to a timeframe of roughly 1–2 weeks, whereas aluminum tooling may demand a month or more for preparation. This contrast highlights the efficiency of these casting methods in speeding the development cycle.

Urethane casting also provides comparative advantages over repeated 3D printing for larger prototype batches. It allows a reduction in per-piece costs and an enhancement in surface finishes, thereby helping with the validation of design iterations prior to the investment in production tooling.

Partnering with local manufacturing entities in Dallas can significantly abbreviate lead times and lower shipping-related delays. A Dallas CNC machine shop, skilled in short run and production machining, can accelerate the transformation of prototypes into finished parts. For those requiring additional finishing, CNC lathe machining Dallas businesses are valued for their precision and consistency in achieving tight tolerances.

Collaboration with a trusted CNC machining company serving Dallas manufacturers ensures the project’s timely completion. Local mold builders and precision shops provide rapid tooling, finishing, and quality assurance services. This combined effort supports both single prototype builds and repetitive production cycles, eliminating the need for protracted delays.

Dallas Tx Cast Inserts Manufacturing Services

Dallas-region production shops integrate mold making, casting, and finishing under one roof, improving production efficiency. They offer silicone mold building for prototypes and compression tooling for short runs. This method supports rapid iteration and supports superior final part quality.

Local Capabilities: Mold Building, Casting, And Finishing

Local Dallas specialists deliver mold building services for manufacturing operations. They are skilled at creating both rubber molds and precision compression molds. Silicone molds are delivered within one to two weeks, making urethane casting valuable for functional prototypes. For metal inserts, die casting or gravity casting is paired with CNC turning and milling to hold precise tolerances.

Advantages Of Choosing A Dallas-Area Supplier Like Lowrance Machine

Lowrance Machine offers integrated workflows that bring together mold building, casting, and post-cast CNC lathe work. This process limits handoffs, promoting consistent results. Customers can use 3–5 axis machining, CMM inspection, and surface treatments, all within the metro area.

How Dallas-Area Supply Improves Lead Times And Shipping

Nearby supply significantly reduces transit time and shipping costs, supporting communication during design and tooling stages. This compresses the loop between engineering and the shop, supporting faster problem-solving for tight schedules. For manufacturers requiring rapid prototypes or small production runs, local cast inserts manufacturing services in Dallas Tx deliver meaningful logistical benefits.

Materials And Processes For High Precision Cast Inserts

Selecting metal and manufacturing process significantly influences the performance, cost, and delivery time of cast inserts. This guide offers an overview of widely used options and the role of secondary operations in meeting precise specifications for complex assemblies.

Common Metal And Alloy Options

Aluminum die cast alloys are commonly chosen for their light weight and resistance to corrosion, making them useful for consumer and electronic components. Stainless steels, including 304 and 316, are preferred for their corrosion resistance in marine and medical applications. Hardened tool steels are well matched to high-wear, load-bearing roles in industrial machinery. Brass and bronze, recognized for their corrosion resistance and ease of machining, are frequently selected in decorative and electrical components.

Casting Methods And Prototype Molding

Aluminum die casting, investment casting, and gravity casting are commonly used for metal inserts requiring mechanical strength. Urethane casting with silicone molds offers a speedy and practical solution for prototypes and small batches. This method allows for the validation of form and fit without the expense of aluminum or steel tooling. Suppliers in Dallas often deliver low-volume silicone mold options, accelerating development timelines.

Secondary Finishing And Machining

Following the casting process, precision machining tightens tolerances and improves surface quality. Common secondary operations include milling, turning, drilling, slotting, and thread rolling. Surface treatments such as plating or passivation can lengthen the lifespan of components in harsh environments. Local machine shops in Dallas employ advanced CNC lathe machining and multi-axis milling to hold stringent specifications, as shown by industry leaders like DyCast and Lakeside Screw Products.

Tradeoffs And Selection Guide

Urethane casting often proves economical for small runs, providing a balance of cost and speed. For larger production volumes, metal casting combined with secondary machining can lower costs per unit and enhance mechanical properties. Engineers must consider material properties, expected wear, and necessary post-casting operations to meet final specifications.

Custom Applications In Dallas

When sourcing custom cast inserts in Dallas, manufacturers can combine both mold builders and precision shops. Combining resources for compression molds in Dallas with full metal casting and CNC lathe machining supports a smooth transition from concept to production.

Tooling And Mold Building For Cast Insert Production

Tooling selection plays a major role in the cost, lead time, and quality of cast inserts. Local expertise enables rapid iteration and limits waste. An experienced mold builder in Dallas for custom tooling solutions offers practical design options. These options help prevent defects, simplify part release, and extend tool longevity.

The Role Of Local Mold Makers

Involving skilled tooling partners in Dallas during design reviews is valuable. They recommend draft angles, venting, and radii that support fill quality and reduce porosity. These changes decrease scrap and expedite production approval.

Silicone And Compression Options

Silicone tooling is ideal for rapid, cost-effective urethane casting prototypes. They help teams to validate form and fit within a short one-to-two-week window. Conversely, compression molds are used for rubber parts, where controlled pressure is needed for elastomer flow and cure. Shops offering rubber molds Dallas and compression molds Dallas facilitate short runs and functional prototypes without significant upfront costs.

Elastomer Tooling Versus Aluminum And Steel

Aluminum or steel production tools are appropriate for high-volume injection or die casting, emphasizing durability and consistency. These tools require longer lead times and higher initial investments. However, they deliver a lower per-part cost at scale and superior surface finish for machining and plating.

Lead Time And Cost Tradeoffs

Prototype mold decisions emphasize speed. Silicone tools typically deliver samples in one to two weeks. In contrast, aluminum or steel tooling may take four to eight weeks, based on complexity. The right choice comes down to balancing run quantity, geometric complexity, and finish requirements.

Mold Building And Manufacturing Integration

Integrated mold building services in Dallas for production needs bring together master pattern making, tool trials, and maintenance plans. Working with local providers lowers shipping time and streamlines revisions during development. This supports a more predictable transition from prototype to production.

Post-Cast Operations And CNC Machining

The process of refining cast inserts requires meticulous machining and rigorous inspection. Dallas-based local shops employ a combination of turning, milling, and measurement techniques. This process transforms raw castings into components of exceptional accuracy. Such work supports that parts satisfy stringent standards of diameter, concentricity, and thread quality, meeting the demands of aerospace, medical, and industrial sectors.

Accurate Lathe Finishing

Using modern lathes, turning and single-point threading make possible the creation of parts with consistent thread form and concentric bores. These shops, experienced with CNC lathe machining services in Dallas, produce both prototype batches and volume production. Their ability to prepare fast and maintain consistent cycle times highlights their commitment to precision.

Multi-Axis Milling For Intricate Components

Advanced five-axis machining centers are used to support handling parts with challenging geometries and multi-face features, reducing the need for multiple fixtures. Regional suppliers, supported by such advanced machinery, support clients in Dallas who require parts with undercuts, compound angles, or simultaneous five-sided machining.

Inspection And Surface Verification

CMM systems play a central role in validating critical dimensions and geometric tolerances. These machines, along with thread gauging, surface finish testing, and statistical sampling, guide quality assurance initiatives. Such measures are used to lower scrap and rework, enhancing overall efficiency and product quality.

Production Step Inspection Capability Typical Use
Lathe turning Precision threading, diameter control, concentricity to 0.0005″ Inside and outside threads on brass, bronze, and aluminum inserts
5-axis milling Intricate contours, indexed faces, and one-setup precision Undercuts, angled faces, and multi-feature cast inserts
Coordinate inspection 3D inspection, tolerance verification, and dimensional documentation Acceptance checks for aerospace, medical, and critical components
Surface verification Ra measurement, polishing, and coating prep Surface finish confirmation for functional and cosmetic assemblies
Comprehensive quality protocols 100% inspection or sampling plans, documented traceability High-reliability runs where every insert must meet spec

Choosing a reputable CNC machine shop in Dallas simplifies the transition from casting to final machining. Such partnerships with CNC machining experts serving Dallas texas manufacturers ensure that tooling selections and inspection protocols fit the specific requirements of the end-use application.

Insert Integration And Custom Fasteners

Pairing cast inserts with matching fasteners strengthens assembly efficiency and extends part lifespan. Engineers in Dallas closely compare insert geometry, thread forms, and material with fastener suppliers. This helps prevent galling and controls installation torque. Local collaboration speeds iteration, ensuring parts meet production goals.

How Matched Component Suppliers Support Insert Projects

Partnering with a custom fastener manufacturer in Dallas helps ensure thread, size, and finish alignment with insert designs. Regional fastener shops and precision machine shops support matched solutions for various fastener types. Yardley Inserts reflects the coexistence of standard and custom items in high-volume production.

Important Design Considerations For Reliable Assemblies

Material matching and thermal movement are key when specifying inserts and fasteners. Thread engagement length, installation method, and corrosion protection are necessary for long-term reliability. Assembly processes must establish installation torque and retention methods, especially for vibration resistance.

Examples In Industrial Use

Custom cast inserts in Dallas are used in electronics housings, furniture joints, medical device assemblies, and heavy marine fittings. Examples include stuffing tubes and heavy-duty ship components, illustrating large-scale applications. Precision shops deliver secondary machining and matched fasteners, supporting parts are ready for assembly.

Use Case Threaded Insert Type Fastener Pairing Core Design Considerations
Electronic housings Threaded brass insert Metric machine screws, M2 through M4 Controlled torque, EMI concerns, and low thermal expansion
Furniture assembly Zinc die-cast insert Hex bolts, captive screws High pull-out strength, flush finish, aesthetic plating
Medical components Precision stainless steel insert Self-clinching fasteners, threaded studs Corrosion resistance, biocompatibility, and exact torque specifications
Saltwater hardware Bronze threaded cast insert Heavy-duty bolts, threaded fittings Long service life, saltwater protection, and fatigue resistance

Working with a custom fastener manufacturer in Dallas and early specification of custom fasteners improve design convergence. This strategy cuts down rework and supports retention under load. Local partnerships promote efficient testing and qualification for production programs.

Complete Supplier Capabilities For Turnkey Services

A full-service supplier managing the entire process streamlines schedules and raises part quality. Local manufacturers can move from CAD models to finished hardware smoothly, removing the need to manage multiple vendors. This approach streamlines the approval process, shortens iteration cycles, and reduces risks for projects with tight deadlines.

Start-To-Finish Manufacturing Services

Engineering support and prototype work form the foundation for dependable parts. Rapid 3D printing for masters and precision mold building prepare for urethane or die casting runs. CNC finishing and inspection support customers receive inserts ready for installation.

Lowrance Machine Service Offerings

Lowrance Machine provides mold building, casting, precision machining, and inspection under one roof. This integrated model facilitates a smooth transition from prototype to short-run production with consistent tolerances. Lowrance Machine supports shop floor scheduling, balancing volumes and delivery windows.

Choosing The Right CNC Shop

Choosing a trusted CNC machine shop in Dallas for custom machined parts cuts down handoffs and improves problem resolution. A reliable CNC machining company serving Dallas manufacturers provides machining expertise, robust quality control, and rapid response to design updates.

Choosing turnkey cast insert services and local expertise significantly reduces lead times and helps keep projects within budget. Suppliers that integrate casting and machining capabilities create a single point of contact for engineering changes, inspection data, and delivery coordination.

Industrial Machine Repair And Maintenance For Production Stability

Supporting production schedules for cast inserts hinges on the efficiency of machine maintenance. Dallas-based localities deliver on-site technicians and comprehensive shop rebuilds. These services are built to minimize downtime, ensuring mold making, casting, and CNC finishing processes remain uninterrupted.

Importance Of Rapid Service To Avoid Downtime

Unforeseen interruptions can badly affect delivery schedules and raise operational costs. The quick involvement of industrial machine repair specialists in Dallas is important. It helps ensure uninterrupted production shifts and prevents the accumulation of workloads. Furthermore, preventive maintenance agreements are important for averting emergency situations by detecting potential issues before they become full-blown failures.

How Maintenance Supports Quality And Lead Times

Consistent quality and predictable lead times are directly correlated with the regularity of maintenance activities. Tasks such as alignment, spindle tuning, and tool-offset checks are important to maintaining dimensional precision in machined inserts. Additionally, the routine servicing of presses and grinding equipment is necessary to sustaining surface finish and tolerances, thereby ensuring that production timelines remain consistent and scrap rates are minimized.

Manufacturer Repair And Field Service Options

Industrial service providers in Dallas delivers a range of services, including machine tool rebuilding, field machining, on-site alignment, spindle repair, and parts support. These full-service industrial equipment and machine repair services in Dallas, Texas, are intended to extend the lifespan of machinery and support its return to operational status.

Finding Service That Supports Production Needs

Before hiring a service provider, it is important to evaluate response times, spare-parts availability, and the provider’s experience with similar equipment. Using a service that combines industrial machine repair services in Dallas, Texas, with preventive maintenance programs is important. This service model helps ensure that manufacturers can meet their deadlines without compromising on the quality of their products.

Selecting A Dependable Cast Inserts Manufacturing Partner

Choosing a vendor should be based on their proven track record in cast insert production and their ability to swiftly transition from tooling to machining. Choose a partner that combines mold creation, casting, and CNC finishing within a single facility. A precision machine shop in Dallas, renowned for industrial components, should boast documented quality assurance processes. These include CMM inspections, first-article reports, and traceable records, thereby lowering risk and supporting the qualification phase.

It is imperative to seek a vendor that shares transparent cost and lead-time comparisons. This transparency is important when deciding between silicone or urethane tooling versus aluminum and steel. For smaller production runs, silicone tooling presents a cost-effective solution with a reduced lead time. Conversely, for larger volumes, aluminum or steel molds deliver superior durability and tighter tolerances.

Before selecting a supplier, request references, sample parts, and inspection reports. A reputable machine shop in Dallas, trusted by industry leaders, will offer a detailed roadmap from prototype to production. They should also showcase their past collaborations with insert specialists, such as Yardley Inserts, to affirm their industry standing. Request specific details on turnaround times, anticipated scrap rates, and planned inspection protocols to accurately evaluate different vendors.

Think about the value of partnering with a local entity like Lowrance Machine, which delivers seamless integration of mold building, casting, and precision machining. A local partner can meaningfully cut shipping times, make possible easier on-site visits, and accelerate the iteration process for Dallas manufacturers. Ultimately, choose vendors with robust quality systems, comprehensive capabilities, and a transparent plan for tooling and volume to help deliver a smooth transition from prototype to production.

Related: Equipment Monitoring by Construction Security Guards in Dallas

Cost-Effectiveness of Using Fibers in Metal Tubes for Industrial Cabling

Unexpected fact: above 70% of new U.S. broadband builds now use fiber networks that demand precise manufacturing to hit performance goals. From material selection through final test reports, Shanghai Weiye OFC Equipment manages FTTH manufacturing to deliver 100% quality assurance.

Our drop designs support aerial, underground, and direct-buried installation, with LSZH, PVC, and PE jacket options and configurations from 1–4 cores. We offer OS1/OS2 and OM2–OM4 grades plus G.652D and G.657 variants, Pantone sheath colors, and logo printing.

SZ Stranding Line

Fiber Secondary Coating Line

Compact Fiber Unit

Computer-controlled machines and advanced equipment keep line speed steady and repeatability reliable. Standard production windows are usually 4–5 days for orders below 100 km and 7–10 days below 500 km, supported by a 1 km MOQ and free replacement warranty for confirmed quality issues.

Read on to see how materials, testing, and support work together to lower lifecycle cost and match the right product to your network system.

Main Takeaways

  • End-to-end manufacturing and laboratory testing support U.S. deployment requirements.
  • Multiple jacket choices and fiber grades serve varied installation environments.
  • Automated equipment helps deliver repeatable quality and dependable optical performance.
  • Fast lead times, low MOQ, and brand fiber options simplify procurement planning.
  • Comprehensive test reports and warranty support product reliability and documentation needs.

Professional FTTH Manufacturing By Shanghai Weiye OFC Equipment

Where project timelines and performance matter, Shanghai Weiye OFC Equipment provides tailored drop solutions with full test documentation.

Shanghai Weiye OFC Equipment works as a focused supplier and manufacturer, pairing specialized equipment with strict material control. We offer customized service and products for residential and MDU rollouts. Each order includes full quality assurance and complete test reporting.

Our lab conducts high-temperature, salt spray, and vibration tests to verify durability. Available jacket choices include LSZH, PVC, and PE. Design options include bow-type flat and self-supporting styles, with brand fibers such as Fujikura and Corning SMF-28e available.

  • Documented line control and production checks for auditable shipments.
  • Engineering assistance covers specifications, sample trials, and volume ramp-up.
  • Modern fixtures and calibration reduce variability so every cable meets operator standards.

Fiber Secondary Coating Line

FTTH Cable Production

At Shanghai Weiye OFC Equipment, manufacturing steps are matched to network specifications, combining brand fiber choices with strict test routines.

Optical Fiber Selection And Brand Options

We select optical fiber to bend radius, attenuation, and deployment type. Available options include OS1, OS2, OM2–OM4, ITU-T G.652D, and G.657.A1/A2. Brand fibers such as Fujikura and Corning SMF-28e are available to meet procurement standards.

Strength Member Installation

Strength members use dielectric FRP or metallic steel wire. FRP works well where non-conductive cable runs are needed. Steel wire adds tensile strength for longer aerial spans and grounding needs.

Jacket Extrusion And Process Control

Jacket options include LSZH for indoor flame safety, PVC for flexibility, and PE for outdoor UV and moisture resistance. Careful control of temperature and capstan ratios helps stabilize line speed and maintain dimensional tolerances.

Cable Component FRP Strength Member Steel strength wire
Best use Non-conductive runs Long aerial spans, higher tensile needs
Main benefit Low weight and non-reactive Greater pulling strength
Installation note Easier terminations May require bonding and grounding

In-Process And Final Testing

Geometry and concentricity checks are performed inline during manufacturing. Final optical tests verify attenuation and return loss. Every order ships with a complete test report plus lab results from high-temperature, salt-spray, and vibration trials to support drop termination and field-use requirements.

Typical lead times are under 100 km in 4–5 days and under 500 km in 7–10 days. Material lot tracking and first-article approvals help support traceability and compliance for U.S. projects.

FTTH Drop Cable Types, Designs, And Structures

Shanghai Weiye OFC Equipment manufactures a compact portfolio of drop designs that serve both tight indoor routes and exposed aerial spans. Every option combines tested materials with geometry designed for field termination and stable optical performance.

Bow-Type Flat Cable For Indoor Distribution

Bow-type flat drop cable keeps the footprint small for risers, hallways, and conduit runs. The design helps maintain low bend loss for easier routing through hallways and MDUs.

Self-Supporting Designs For Aerial Spans

Self-supporting FTTH drop designs use a messenger element to handle tensile loading. Dielectric FRP is available for non-conductive routes, while steel wire is suitable when bonding and additional tensile strength are needed.

Strength Members And Core Layouts

We offer dielectric and metallic strength member configurations to match safety and EMI rules. Center loose tube and unitube flat types balance crush resistance and fiber access for quick termination.

Jacket Choices For Indoor And Outdoor Use

Jacket options include LSZH for flame-retardant, low-smoke indoor applications and PE for outdoor UV and moisture resistance. Every cable family is checked for mechanical and optical quality before shipment.

Cable design Recommended use Support member Sheath
Bow-type flat Indoor risers, MDUs Non-metallic FRP LSZH
Aerial self-supporting Outdoor aerial routes FRP or steel wire Outdoor PE
Center loose tube Higher fiber counts FRP LSZH/PE
Flat unitube Simple stripping applications Steel wire or FRP LSZH or PE sheath

Production Line Equipment For Quality And Speed

Automation and sensor-driven feedback at Shanghai Weiye OFC Equipment limit manual handling and improve throughput for patch cord prep.

The production line uses automated cutting and stripping machines for drop patch cords, helping increase throughput and reduce labor variation.

The CLX-BPO2 auto-stripping machine works under PLC and photoelectric control. With a cycle time of about 1.5 seconds, it supports real-world speeds near 20 terminal operations per minute.

Drop Cable Patch Cord Cutting And Stripping Automation

The equipment can strip LSZH and PVC jackets while trimming FRP or steel strength members to accurate stub lengths. Cylinder-driven actuators deliver fast, repeatable motion and low downtime.

PLC And Photoelectric Control For Precision And Repeatability

PLC logic combined with photoelectric sensors provides accurate positioning and closed-loop control. Inline checks feed control charts so operators can correct trends before defects grow.

Function Capability Result
Auto-stripping machine Fast cycle and automated stripping ~20 terminals/minute throughput
Motion system Cylinder-based High speed and reliability
Material handling LSZH/PVC; FRP/steel Cleaner termination readiness
Control method PLC control, sensors, and inline checking Consistent quality, lower rework
  • Automatic waste ejection and ergonomic loading help keep the work area clean.
  • Control plans record calibration intervals and key operating parameters.
  • Machines, fixtures, and trained staff work together to meet FTTH volume goals while preserving accuracy.

CLX-BPO2 Auto-Stripping Machine Functions In Our Line

The CLX-BPO2 brings industrial-grade stripping and trimming to our line, cutting cycle time while keeping prep consistent.

Shanghai Weiye OFC Equipment uses the CLX-BPO2 to increase output while standardizing terminal preparation quality. The unit runs at an approximate cycle time of 1.5 seconds, yielding about 20 terminal preparations per minute in production.

PLC and photoelectric controls provide accurate detection and repeatable machine movement. That control helps keep strip lengths and reserved strength stubs within tight tolerances.

Cycle Time And Throughput

Normal operating speed is about 1.5 seconds per cycle. That speed translates into steady throughput during continuous production.

Supported Jacket And Reserved Strength Lengths

The CLX-BPO2 can strip LSZH and PVC jackets, with adjustable jacket strip length from 17.5 to 35.0 mm. Reserved strength member stubs are set between 7.0 and 11.0 mm to match common termination hardware.

Handling FRP And Steel Wire Strength Members

The machine cuts FRP and steel wire strength elements cleanly while helping protect nearby fibers. Customized cutters are available for nonstandard sizes to preserve precision.

  • Automatic waste ejection and sensor-triggered starting help reduce idle time.
  • A compact size of L40 × W18 × H18 cm, 110–220V power, 50W rating, and 11 kg weight make workcell integration easier.
  • Cylinder-driven motion and PLC/photoelectric control improve line reliability and lower maintenance interruptions.
Specification Value Production benefit
Operating cycle About 1.5 s, around 20/min High throughput for production runs
Adjustable strip length (A) Adjustable 17.5–35.0 mm Supports common connector prep
Strength stub (B) Adjustable 7.0–11.0 mm Supports strength and termination requirements
Power and dimensions Compact 110–220V, 50W machine Easy integration into existing equipment

Using this machine, Shanghai Weiye OFC Equipment controls prep so field teams receive drop parts ready for quick installation. The CLX-BPO2 supports production volume targets while helping maintain quality.

Custom Specifications To Match Your FTTH System

Shanghai Weiye OFC Equipment configures each build to meet your network requirements and simplify field rollout. We pair concise options with predictable manufacturing windows so your teams receive ready-to-install products.

Core Counts, Fiber Choices, And Cable Colors

Choose 1–4 core designs with single-mode or multimode fiber. Options include OS1, OS2, and OM2–OM4 plus G.652D and G.657 variants to match your optics and connector plans.

We match sheath colors to Pantone codes for fast field ID and consistent asset tagging.

Jacket Choices, Print Legends, And Logos

Select LSZH, PVC, or PE jackets based on route and safety rules. Custom print legends and logos support inventory and warranty tracking.

Length Choices, Packaging, And Custom Structures

Standard lengths include 1 km, 2 km, and 4 km, with customized reels and packaging for storage and handling needs. Bow-type flat or self-supporting designs can be paired with steel wire or FRP strength members to match span, bonding, and isolation requirements.

Specification option Typical choice Practical benefit
Put-up length 1 km, 2 km, or 4 km Reduced staging and simpler reel handling
Sheath LSZH, PVC, or PE Indoor/outdoor compatibility
Cable structure Bow-type flat or self-supporting More routing and span options

As a supplier, Shanghai Weiye coordinates production with your schedule and provides documentation listing final specifications for easier on-site QA.

Quality Assurance, Testing, And Documentation

Shanghai Weiye OFC Equipment builds quality checkpoints into the production line so each item ships with documented acceptance data.

Laboratory Testing For Heat, Salt Spray, And Vibration

Our lab runs high-temperature exposure, salt spray corrosion, and vibration tests to qualify materials and assemblies. These tests recreate field stresses for indoor and outdoor use.

100% Test Reports For Every Cable

Every fiber optic cable ships with a 100% test report that logs attenuation, return loss, and geometry where applicable. Final inspection checkpoints prevent nonconforming items from leaving the factory.

Compliance And Traceability

Batch records tie test data to reels and serials so audits and warranty claims are simple to verify. Documentation follows common customer templates to speed approvals and inbound inspection.

  • Line checks and final inspection prevent field failures and lower warranty events.
  • QA packages include specifications confirmation and formatted test data for rapid review.
  • Ongoing test trends guide preventive maintenance and improve long-term reliability.
Test Testing purpose Result
Heat exposure Material stability Validated heat endurance
Corrosion exposure Corrosion resistance Verified outdoor readiness
Vibration Resistance to handling stress Improved field reliability

FTTH Drop Cable Pricing And Cost Drivers

Budgeting for a drop run starts with fiber and jacket choices and is refined by volume and customization.

Pricing can vary widely, from about $30 to $1,000 per unit, depending on fiber grade, jacket material, length, and structure.

Material Choices, Fiber Grade, Jacket Type, And Structure

Main cost drivers include fiber optic grade, jacket material, and the cable structure selected for deployment.

Self-supporting designs and steel strength elements raise material and labor input. Custom colors, logos, and print legends add setup time and influence price for short runs.

Price Impact Of Length, Volume, And Custom Options

Longer reel lengths and larger-volume orders usually reduce unit cost. Smaller quantities often involve setup fees and higher per-unit pricing.

  • Machine changeovers and special cutters can increase lead time and cost.
  • Clear RFQs and line scheduling let Shanghai Weiye OFC Equipment align price quotes to delivery windows.
  • Framework agreements and indexed pricing can help stabilize budgets across rollout phases.
Cost factor Effect on price Recommendation
Optical fiber grade Strong influence Avoid over-specifying when possible
Jacket type Moderate impact Compare LSZH vs. PE for total cost
Cable quantity and reel length Large impact Consolidate runs to cut unit cost

Lead Times, MOQ, And Delivery For The United States

Shanghai Weiye OFC Equipment makes lead times and logistics clear so planners can align crews and sites. Predictable windows reduce downtime and help control cost when a rollout is underway.

Typical Production Windows And Capacity Planning

Typical production windows are 4–5 days for orders below 100 km and 7–10 days for orders below 500 km. Line capacity is scheduled around rollout milestones to support on-time delivery.

The service team issues production updates and tracking so installation teams know when reels arrive. For tight schedules, we hold contingency capacity to accelerate critical-path orders.

MOQ And Why It Matters

The minimum order quantity is 1 km. This reflects setup needs such as wire and jacket die adjustments that consume start-up material and scrap.

Length and staging plans are reviewed to choose reel sizes that reduce waste and handling. Batch releases can balance inventory carrying costs with more frequent, smaller job-site deliveries.

Installation Readiness And Application Scenarios

Site conditions dictate whether a self-supporting span, duct pull, or direct-buried run is the best fit for a project.

Aerial, Duct, And Direct-Buried Installation Considerations

For aerial runs, Shanghai Weiye OFC Equipment recommends self-supporting designs with correct strength members to control sag and tension for long-term reliability.

Duct installations perform best with low-friction jackets and crush-resistant constructs so pulling does not damage fibers. PE jackets are common for underground and buried paths where moisture resistance matters.

Direct-buried designs require proper depth control per local codes and moisture-resistant jackets to protect the optic core over time.

Indoor Riser And Plenum Distribution With ONT Termination

Indoor riser and plenum routes favor LSZH jackets to meet flame and smoke rules. Flat drop cable forms strip cleanly and present controlled strength stubs for quick ONT termination.

We guide the choice of steel or FRP (dielectric) strength members based on bonding needs, lightning exposure, and hardware compatibility. Standardized production-line preparation helps shorten installation time and reduce scrap.

Application Important feature Field note
Aerial span Self-supporting, steel or FRP Check tension and messenger hardware
Duct Low-friction jacket, crush resistance Use pull tape and proper lubricant
Buried route Outdoor PE moisture protection Follow local depth and warning tape rules
Indoor distribution LSZH sheath with bend control Maintain bend radius at wall penetrations

This approach supports consistent installation across indoor and outdoor transitions. The result is fewer callbacks, faster activations, and more dependable field performance for the system.

End-To-End Support And After-Sales Service

The team coordinates testing, line scheduling, and installation guidance to reduce surprises during deployment.

Shanghai Weiye OFC Equipment provides engineering support from early requirements through approved drawings and pre-production builds. Documentation templates and clear installation notes help field crews work from a consistent plan.

After-sales service covers rapid response, root-cause analysis, and corrective actions. Every product ships with full test reporting and traceability to support QA acceptance.

  • Round-the-clock availability supports status updates and technical guidance.
  • Warranty with free replacement if any quality problems are confirmed.
  • Line schedule coordination helps handle urgent changes and acceleration requests.
  • Configuration control so shipped items match agreed requirements every time.
Support area Service provided Customer benefit
Engineering Specification review and pre-production builds Cleaner rollout planning
Lab testing Lab trials & 100% test reports Documented product quality
After-sales Rapid replacement & root-cause Faster issue resolution

Summary

Shanghai Weiye OFC Equipment is a strong choice for customized drop builds, short production windows, and traceable quality documentation.

We deliver customized ftth drop solutions that pair material choices with validated manufacturing and lab testing. Every reel ships with a 100% test report and documented trials to support field acceptance in the United States.

A strong production line, including CLX-BPO2-enabled preparation machines, reduces variation and improves turnaround. Our equipment standardizes strip lengths and strength stubs so installers receive consistent results during turn-up.

From fiber selection through jacket, printing, and packaging, we balance design and cost to support longer service life. Dedicated support guides scheduling, logistics, and after-sales care so your deployment stays on plan.

Contact Shanghai Weiye OFC Equipment to align specs, timeline, and volume. We stand behind every fiber optic and optic cable shipment with lab validation and responsive service.

Related: Mechanical Stress Testing for Fibers in Metal Tubes

How an SZ Stranding Line Supports Loose Tube and Ribbon Cable Designs

Above 65% of recent broadband deployments in metropolitan U.S. projects now require fiber-to-the-home. This accelerated move toward full-fiber networks highlights the immediate need for dependable production equipment.

Compact Fiber Unit
Fiber Secondary Coating Line

Shanghai Weiye Optic Fiber Communication Equipment Co (www.weiye-ofc.com) delivers automated FTTH cable production line systems for the United States market. Their turnkey FTTH Cable Production Line for High-Speed Fiber Optics brings together machines and control systems. It produces drop cables, indoor/outdoor cables, and high-density units for telecom, data centers, and LANs.

This modern FTTH cable making machinery offers measurable business value. This line offers higher throughput and consistent optical performance using low attenuation. It additionally aligns with IEC 60794 and ITU-T G.652D / G.657 standards. Customers see reduced labor costs together with material waste through automation. Full delivery services cover installation as well as operator training.

The FTTH cable production line package contains fiber draw tower integration, a fiber secondary coating line, and a fiber coloring machine. It also includes SZ stranding line, fiber ribbone line, compact fiber unit assembly, cable sheathing line, armoring modules, and testing stations. Control and power specs typically use Siemens PLC with HMI, operating at 380 V AC ±10% and modular power consumption up to roughly 55 kW depending on configuration.

Shanghai Weiye’s customer support model covers on-site commissioning by experienced engineers, remote monitoring, and rapid troubleshooting. It also includes lifetime technical support and operator training. Clients are usually asked to coordinate engineer logistics as part of standard supplier practice when ordering from FTTH cable machine suppliers.

Key Takeaways

  • FTTH production line systems meet growing U.S. demand for fiber-to-the-home deployments.
  • Complete turnkey systems from Shanghai Weiye combine automation, standards compliance, and operator training.
  • Modular setups use Siemens PLC + HMI and operate near 380 V AC with up to ~55 kW power profiles.
  • Built-in modules cover drawing, coating, coloring, stranding, ribbone, sheathing, armoring, and testing.
  • Advanced FTTH cable making machinery reduces labor, waste, and improves optical consistency.
  • Service coverage includes on-site commissioning, remote diagnostics, and lifetime technical assistance.

SZ stranding lines

Understanding FTTH Cable Line Technology

The fiber optic cable manufacturing process for FTTH requires precise control at every stage. Manufacturers employ integrated lines that combine drawing, coating, stranding, as well as sheathing. That setup boosts yield together with speeds up market entry. This system meets the needs of both residential together with enterprise deployments in the United States.

Here, we summarize the core components and technologies driving modern manufacturing. Each module must operate with precise timing and reliable feedback. The choice of equipment affects product quality, cost, and flexibility for various cable designs.

Modern Fiber Optic Cable Manufacturing Components

Secondary coating lines apply dual-layer coatings, often 250 µm, using high-speed UV curing. Tight buffering as well as extrusion systems produce 600–900 µm jackets for indoor together with drop cables.

SZ stranding lines use servo-controlled pay-off and take-up units to handle up to 24 fibers with accurate lay length. Fiber coloring machines employ multi-channel UV curing to mark fibers to industry color codes.

Sheathing together with extrusion stations form PE, PVC, or LSZH jackets. Armoring units add steel tape or wire for outdoor protection. Cooling troughs and UV dryers stabilize profiles before testing.

How Production Systems Evolved From Traditional To Advanced

Early plants used manual as well as semi-automatic modules. Lines were separate, with hand transfers together with basic controls. Advanced facilities move to PLC-controlled, synchronized systems with touchscreen HMIs.

Remote diagnostics as well as modular turnkey setups support rapid changeover between simplex, duplex, ribbon, and armored formats. That shift supports automated fiber optic cable production together with lowers labor dependence.

Key Technologies Powering Industry Innovation

High-precision tension control, based on servo pay-off as well as take-up, keeps geometry stable during fast-cycle runs. Multi-zone temperature control using Omron PID together with precision heaters helps ensure consistent extrusion quality.

High-speed UV curing as well as water cooling improve profile stabilization while reducing energy use. Integrated inline testers measure attenuation, geometry, tensile strength, crush resistance, together with aging data.

Process Typical Module Key Benefit
Fiber draw process Automated draw tower with tension feedback Consistent core diameter and low attenuation
Secondary coating Dual-layer UV coaters Consistent 250 µm coating for durability
Fiber coloring Multi-channel fiber coloring machine Precise identification for splicing and installation
Stranding SZ line with servo control for up to 24 fibers Stable lay length for ribbon and loose tube designs
Extrusion & sheathing Energy-saving extruders with multi-zone heaters PE/PVC/LSZH jackets with tight dimensional control
Protection armoring Steel tape or wire armoring units Stronger mechanical protection for outdoor applications
Cooling and curing Water troughs and UV dryers Fast profile stabilization and reduced defects
Inline testing Real-time attenuation and geometry measurement Live quality control and compliance reporting

Compliance with IEC 60794 and ITU-T G.652D/G.657 variants is standard. Manufacturers typically certify to ISO 9001, CE, and RoHS. These credentials support diverse applications, from FTTH drop cable production to armored outdoor runs and data center high-density solutions.

Choosing cutting-edge fiber optic line output equipment as well as modern manufacturing equipment enables firms meet tight tolerances. Such equipment selection enables efficient automated fiber optic cable manufacturing and positions companies to deliver on scale together with quality.

Key Equipment For Fiber Secondary Coating Line Operations

The secondary coating stage is critical, giving drawn optical fiber its final diameter and mechanical strength. It prepares the fiber for stranding and cabling. A well-tuned fiber secondary coating line controls coating thickness, adhesion, together with surface output quality. This protects the glass during handling.

Producers aiming for high-yield, high-speed fiber optic cable production must match material, tension, and curing systems to process requirements.

High-speed secondary coating processes rely on synchronized pay-off, coating heads, as well as UV ovens. Current systems achieve high manufacturing rates while minimizing excess loss. Precise tension control at pay-off together with winder stages prevents microbends and supports consistent coating thickness across long runs.

Single and dual layer coating applications serve different market needs. Single-layer setups provide basic mechanical protection and a simple optical fiber cable production machine footprint. Dual-layer lines combine a harder inner layer with a softer outer layer to improve microbend resistance and stripability. This helps when fibers are prepared for connectorization.

Temperature control and curing systems are critical to final fiber performance. Multi-zone heaters and Omron PID controllers guide screw/barrel extruders to stable melt flow for LSZH or PVC compounds. UV curing ovens and water trough cooling stabilize the coating profile and reduce variation in excess loss; targets for high-quality single-mode fiber often aim for ≤0.2 dB/km at 1550 nm after extrusion.

Key components from trusted suppliers improve uptime as well as precision in an optical fiber cable manufacturing machine. Extruders such as 50×25 models, screws as well as barrels from Jinhu, together with bearings from NSK are common. Motors from Dongguan Motor, inverters by Shenzhen Inovance, as well as PLC/HMI platforms from Siemens or Omron deliver robust control together with monitoring for continuous runs.

Operational parameters guide preventive maintenance and process tuning. Typical pay-off tension ranges from 0.4 to 1.5 N for fiber reels, while radiation and curing speeds are adjusted to material type and coating thickness. A preventive maintenance cycle around six months keeps secondary coating processes stable and supports reliable high-speed fiber optic cable production.

Fiber Draw Tower And Preform Processing

The fiber draw tower is the core of optical fiber drawing. It softens a glass preform in a multi-zone furnace. Then, it pulls a continuous strand with precise diameter control. That stage sets the refractive-index profile and attenuation targets for downstream processes.

Process control on the tower relies on real-time diameter feedback together with tension management. This prevents microbends. Cooling zones as well as closed-loop systems keep geometry stable during the optical fiber cable manufacturing process. Current towers log metrics for traceability together with rapid troubleshooting.

Output quality supports single-mode fibers such as ITU-T G.652D and bend-insensitive types like G.657A1/A2 for FTTH networks. Draws routinely meet stringent loss figures. Excess loss after coating is kept at or below 0.2 dB/km for high-performance single-mode fiber.

Integration with secondary coating lines requires careful pay-off control. A synchronized handoff preserves alignment and tension as the fiber enters coating, coloring, or ribbon count stations. This link ensures the optical fiber drawing step feeds smoothly into cable assembly.

Equipment vendors such as Shanghai Weiye offer turnkey options. These include testing stations for attenuation, tensile strength, and geometric tolerances. These integrated features help manufacturers scale toward high-speed fiber optic cable manufacturing while maintaining ISO-level output quality checks.

Key Feature Main Purpose Typical Goal
Multi-zone furnace Even preform heating for stable glass viscosity Stable draw speed and refractive profile
Real-time diameter control Maintain core/cladding geometry and reduce attenuation ±0.5 μm tolerance
Managed tension and cooling Prevent microbends and control fiber strength Target tension based on fiber type
Automatic pay-off integration Secure handoff to secondary coating and coloring Synced feed rates for zero-slip transfer
Integrated online testing stations Check attenuation, tensile strength, and geometry Single-mode loss target of ≤0.2 dB/km after coating

Advanced SZ Stranding Line Technology In Cable Assembly

The SZ stranding method creates alternating-direction lays that cut axial stiffness and boost flexibility. That makes it ideal for drop cables, building drop assemblies, and any application that needs a flexible core. Producers moving toward automated fiber optic cable manufacturing use SZ approaches to meet tight bend as well as axial tolerance specs.

Precision in the stranding stage protects optical performance. Modern precision stranding equipment uses servo-driven carriers, rotors, and modular pay-off racks that accept up to 24 fibers. These systems deliver precise lay-length control and allow quick reconfiguration for different cable types.

Automated tension control systems keep fibers within safe limits from pay-off to take-up. Servo pay-offs, capstans, and haul-off units maintain constant linear speed and target tensions. Typical fiber pay-off tension ranges from 0.4 to 1.5 N while reinforcement pay-offs run between 5 and 20 N.

Integration with a downstream fiber cable sheathing line streamlines production and reduces handling. Extrusion of PE, PVC, or LSZH jackets at 60–150 m/min syncs with stranding through a Siemens PLC. Cooling troughs and UV dryers stabilize the jacket profile right after extrusion to prevent ovality and reduce mechanical stress.

Optional reinforcement and armoring modules add strength without compromising flexibility. Reinforcement pay-off racks accept steel wires or FRP rods. Armoring units wrap steel tape or wire with adjustable tension to meet specific mechanical ratings.

Built-in output quality control prevents defects before cables leave the line. In-line geometry checks, fiber strain monitors, as well as optical attenuation measurement detect excess loss or mechanical strain caused by stranding or sheathing. These checks support continuous automated fiber optic cable manufacturing workflows together with cut rework.

The combination of a robust sz stranding line, high-end precision stranding equipment, and a synchronized fiber cable sheathing line provides a scalable solution for manufacturers. That setup raises throughput while protecting optical integrity and mechanical performance in finished cables.

Fiber Coloring Machines And Identification Systems

Coloring and identification are critical in fiber optic cable production. Accurate color application minimizes splicing errors and accelerates field work. Modern equipment combines fast coloring with inline inspection, ensuring high throughput and low defect rates.

Today’s high-speed coloring technology supports multiple channels and quick curing. Machines can operate 8 to 12 color channels simultaneously, aligning with secondary coating lines. UV curing at speeds over 1500 m/min ensures color and adhesion stability for both ribbon and counted fibers.

The next sections review standards and coding prevalent in telecom networks.

Color coding adheres to international telecom standards for 12-color cycles and ribbon schemes. That consistency aids technicians in installation and troubleshooting. Consistent coding significantly reduces field faults and accelerates network deployment.

Quality control integrates advanced fiber identification systems into production lines. In-line cameras, spectrometers, and sensors detect color discrepancies, poor saturation, and coating flaws. The PLC/HMI interface alerts to issues and can pause the line for correction, safeguarding downstream processes.

Machine specifications are vital for uninterrupted runs as well as material compatibility. Leading equipment accepts UV-curable pigments together with inks, compatible using common coatings as well as extrusion steps. Pay-off reels accommodating 25 km or 50 km spools ensure continuous operation on high-volume lines.

Supplier support is essential for US manufacturers adopting these technologies. Shanghai Weiye and other established vendors offer customizable channels, remote diagnostics, and onsite training. This support reduces ramp-up time and enhances the reliability of fiber optic cable production equipment.

Specialized Solutions For Fibers In Metal Tube Production

Metal tube and metal-armored cable assemblies provide robust protection for fiber lines. They are ideal for direct-buried and industrial applications. The controlled routing of coated fibers into metal tubes prevents microbends, ensuring optical performance remains within specifications.

Processes depend on precision filling and centering units. These modules, in conjunction with fiber optic cable manufacturing equipment, ensure concentric placement and controlled tension during insertion.

Armoring steps involve the use of steel tape or wire units with adjustable tension and wrapping geometry. This method benefits armored fiber cable production by preventing compression of fiber elements. It also keeps reinforcement wires at typical diameters of ø0.4–ø1.0 mm.

Coupling armoring with downstream sheathing and extrusion lines results in a finished outer jacket made of PE, PVC, or LSZH. An optical fiber cable production machine must handle pay-off reels sized for reinforcement and align with sheathing tolerances.

Quality checks include crush, tensile, as well as aging tests to confirm the armor does not exceed allowable stress on fibers. Standards-based testing helps ensure long-term reliability in field conditions.

Turnkey solutions from established manufacturers integrate metal tube handling featuring SZ stranding as well as sheathing lines. These solutions include operator training and maintenance schedules to sustain throughput on fiber optic cable manufacturing equipment.

Buyers should consider compatibility with armored fiber cable production modules, ease of changeover, and service support for field upgrades. Those points reduce downtime and protect investment in an optical fiber cable production machine.

Fiber Ribbon Line And Compact Fiber Unit Production

Modern data networks require efficient assemblies that pack more fibers into less space. Manufacturers employ a fiber ribbon line to create flat ribbon assemblies for rapid splicing. That production method uses parallel processes and precise geometry to meet the needs of MPO trunking and backbone cabling.

Advanced equipment ensures accuracy and speed in production. A fiber ribbon line typically integrates automated alignment, epoxy bonding, precise curing, and shear/stacking modules. In-line attenuation and geometry testing reduce rework, maintaining high yields.

Compact fiber unit manufacturing focuses on tight tolerances and material choice. Extrusion together with buffering create compact fiber unit constructions using typical tube diameters from 1.2 to 6.0 mm. Common materials include PBT, PP, as well as LSZH for durability together with flame performance.

High-density cable solutions aim to enhance rack and tray efficiency in data centers. By increasing fiber count per unit area, these designs shrink cable diameter and simplify routing. They are compatible with MPO trunking and high-count backbone systems.

Production controls and speeds are critical for throughput. Advanced lines can reach up to 800 m/min, depending on configuration. PLC and HMI touch-screen control enable quick parameter changes as well as synchronization across multiple lines.

Quality as well as customization remain key differentiators for manufacturers like Shanghai Weiye. Electronic monitoring, customizable ribbon counts, stacking patterns, together with turnkey integration with sheathing and testing stations support bespoke high-output fiber cable manufacturing line requirements.

Key Feature Fiber Ribbon Line Compact Fiber System Benefit for Data Centers
Typical Speed As high as 800 m/min Around 600–800 m/min Higher throughput for large deployments
Key Processes Alignment automation, epoxy bonding, and curing Extrusion, buffering, and tight-tolerance winding Consistent geometry and lower insertion loss
Primary materials Specialty tapes and bonding resins PBT, PP, and LSZH jackets/buffers Long service life with compliance benefits
Quality testing Real-time attenuation and geometry inspection Dimensional control and tension monitoring Lower failure rates and faster rollout
System integration Integrated sheathing with splice-ready stacking Modular compact units for dense cable solutions Simplified MPO trunking and backbone construction

Optimizing High-Speed Internet Cable Production

Efficient high-speed fiber optic cable production relies on precise line setup and strict process control. To meet US market demands, manufacturers must adjust pay-off reels, extrusion dies, and tension systems. This ensures optimal output for flat, round, simplex, and duplex FTTH profiles.

FTTH Application Cabling Systems

FTTH cabling systems must accommodate various drop cable types while maintaining consistent center heights, like 1000 mm. Production lines for FTTH include 2- and 4-reel pay-off options. They also feature reinforcement pay-off heads for enhanced strength.

Extruder models, such as a 50×25, control jacket speeds between 100 and 150 m/min, depending on LSZH or PVC. Extrusion dies for 2.0×3.0 mm profiles guarantee reliable jackets for field installation.

Fiber Pulling Process Quality Assurance

Servo-controlled pay-off and take-up units regulate fiber tension between 0.4–1.5 N to prevent excess loss. Inline systems conduct fiber pull testing, attenuation checks, mechanical tensile tests, together with crush together with aging cycles. Such tests verify performance.

Key control components include Siemens PLCs and Omron PID controllers. Motors from Dongguan Motor together with inverters from Shenzhen Inovance ensure stable operation as well as easier maintenance.

How Optical Fiber Drawing Meets Industry Standards

A well-tuned fiber draw tower produces fibers that meet ITU-T G.652D together with G.657 standards. This goal is to achieve ≤0.2 dB/km excess loss at 1550 nm for high-consistency single-mode fiber.

Choosing the best equipment for FTTH cables involves evaluating speed, customization, warranty, and local after-sales support. Top FTTH cable production line manufacturers provide turnkey layouts, remote monitoring, and operator training. Such support reduces ramp-up time for US customers.

Closing Summary

Advanced FTTH cable making machinery integrates various components. These include fiber draw towers, secondary coating, coloring lines, SZ stranding, and ribbon units. It also includes sheathing, armoring, and automated testing for consistent high-speed fiber production. A complete fiber optic cable production line is designed for FTTH and data center markets. It enhances throughput, keeps losses low, and maintains tight tolerances.

For U.S. manufacturers and system integrators, partnering with reputable suppliers is key. They should offer turnkey systems with Siemens or Omron-based controls. This includes on-site commissioning, remote diagnostics, and lifetime technical support. Companies like Shanghai Weiye Optic Fiber Communication Equipment Co provide integrated solutions. Such solutions simplify automated fiber optic cable manufacturing and reduce time to production.

Technically, ensure line configurations adhere to IEC 60794 and ITU-T G.652D/G.657 standards. Verify tension and curing settings to meet excess loss targets, such as ≤0.2 dB/km at 1550 nm. Adopt preventive maintenance cycles of roughly six months for reliable 24/7 operation. When planning a new FTTH cable production line, first evaluate required cable types. Collect product drawings and standards, request detailed equipment specs and turnkey proposals, and schedule engineer commissioning and operator training.

Compact Fiber Unit for Buffered Fiber Production

Could the machines manufacturing fiber optic cable production machinery serve as the unseen force that ultimately delivers true gigabit access to every American home? This article explores the recent breakthroughs in FTTH Cable Production Line Technology. These advancements are reshaping broadband network infrastructure and accelerating fiber to the home technology across the United States.

SZ Stranding Line

FTTH Cable Production Line

Fiber Secondary Coating Line

Modern advancements in automation, precision engineering, and AI-driven inspection are substantially lowering production costs and boosting quality. This synergy makes high-speed internet technology more dependable and simpler to deploy for service providers and municipalities.

Global optical cable output now exceeds hundreds of millions of kilometers annually. This surge is fueled by 5G deployments, hyperscale data centers, and the growing demand for streaming and remote work. The subsequent sections will examine automation and Industry 4.0, the use of low-loss materials, AI quality control, innovative cable designs such as bend-insensitive fiber and flat drop microcables, and the pursuit of sustainability in production lines.

Telecommunications manufacturing, network planning, and procurement professionals will gain valuable insights. These insights focus on selecting the right fiber optic cable production machinery and optimizing processes. They are designed to meet regional deployment needs and future bandwidth growth.

FTTH Cable Production Line Technology

The term encompasses the machinery, control systems, and materials transforming optical preforms into deployable fiber cables. It encompasses fiber drawing and coating, SZ stranding, ribbon formation, extrusion of jackets, armoring, taping, automated testing, and final take-up systems. Each step’s precise control defines the fiber optic cable production process, ensuring consistent performance.

The manufacturing chain demands stringent tolerances. SZ stranding systems align dozens of strands with micron-level tension precision. Extrusion lines employ servo-driven extruders and laser micrometers to maintain jacket thickness within ±0.02 mm. Such precision minimizes variability, lowering attenuation and making field splicing easier.

Standards and regulatory frameworks strongly shape manufacturing decisions. Compliance with ITU-T recommendations, such as G.657, and regional fire codes like CPR in Europe, is essential. Meeting these standards ensures products align with the broader broadband network infrastructure.

Quality in production directly impacts network economics and service delivery. Lower attenuation and consistent geometry reduce splice loss and extend reach. This enhances reliability for carriers, ISPs, and utilities, while lowering the total cost of ownership for FTTH deployments. The growing demand for symmetrical multi-gigabit services, 5G backhaul, and data center interconnect is driving the scale-up of modern lines.

Comparing key process components and tolerances reveals their impact on output and quality.

SZ Stranding Line

Process Component Standard Control Impact on Performance
Fiber draw and coating Temperature stability ±1°C; concentricity control ±5 µm Consistent geometry; reduced macrobend loss
Ribbon formation and SZ stranding Micron-level tension regulation; synchronization at 0.5 ms Even fiber pitch; more predictable connector and splice results
Extrusion and jacket thickness Laser micrometer feedback; ±0.02 mm tolerance Reliable mechanical protection; consistent installation response
Tape wrapping and armoring Servo-controlled feed rate; layer alignment control Enhanced crush protection; supports compliant aerial and buried specs
Take-up and automated testing OTDR and insertion loss checks at line speed; tension-controlled winding Complete quality traceability; lower rework and fewer failures in the field

Manufacturers like Corning, Prysmian Group, and Sumitomo Electric focus on tighter process control to meet operator expectations. Continuous advancements in the fiber optic cable production process enable networks to scale while maintaining performance in the last mile of broadband network infrastructure.

Automation And Industry 4.0 In Fiber Optic Cable Production

Factory floors for fiber optic cable production machinery now mirror advanced manufacturing plants from other industries. Smart controls, synchronized stages, and data-driven decision making raise output and protect quality. These shifts shorten commissioning time for new product families. They let telecommunications equipment manufacturers pivot between armored aerial lines and microcable runs with minimal downtime.

Smart machinery and PLC coordination

Programmable logic controllers coordinate stranding frames, ribbon formers, and take-up units to keep tension within sub-0.01mm windows. Servo-driven extrusion coupled with laser micrometers enforce ±0.02mm jacket thickness. The result is fewer rejects, less rework, and consistent optical performance on every reel.

Edge computing and production orchestration

Local edge servers ingest terabytes of telemetry each day. They drive low-latency closed-loop adjustments and push immediate alerts when deviations occur. This approach keeps optical fiber cable equipment running at peak efficiency. It supports real-time quality assurance during long production runs.

AGVs, material flow, and workflow gains

Automated Guided Vehicles move heavy cable drums with millimeter-level repeatability. Laser-navigated AGVs reduce manual handling injuries and speed material flow between extrusion, curing, and drum stations. This automation lowers labor costs while raising throughput on ftth cable production line technology setups.

Advantages for manufacturers and supply networks

  • Increased throughput with consistent results
  • Accelerated prototyping and reduced time to market
  • Less labor risk and lower operational expense
  • Better integration between optical fiber cable equipment and enterprise systems

Adoption across the industry ecosystem

Leading telecommunications equipment manufacturers pair PLCs with robotic arms, AGVs, and industrial IoT stacks to reach Industry 4.0 goals. This integration creates a resilient production base. It is able to adapt as demand shifts toward denser, more complex FTTH offerings.

Precision Engineering Breakthroughs For Lower Attenuation

Advances in materials and mechanical design are driving down loss in modern fiber lines. Engineers pair ultra-low loss fiber with tighter coating control to reduce intrinsic and bending attenuation. These gains matter to network operators who want longer spans and fewer amplifiers in high-speed internet technology deployments.

The fiber optic cable production process now favors smaller coated diameters such as 180µm and 160µm. These sizes let manufacturers increase fiber count and build denser microcables without sacrificing handling or optical stability.

Low-Loss Glass And Advanced Coatings

Manufacturers use improved glass formulations that lower Rayleigh scattering and reduce baseline attenuation. Ultra-low loss fiber variants extend reach for long-haul and high-capacity links while easing repeaters and amplifier requirements.

Coating chemistry has progressed too. UV-cured acrylate systems cut microbending loss by roughly 40% compared with earlier generations. That performance drop helps maintain signal integrity in cramped ducts and tight bends common in FTTH and 5G backhaul networks.

Central Strength Members And Mechanical Design

Mechanical design updates center on robustness and dimensional control. Fiber-reinforced plastic (FRP) rods with tensile strengths near 1.2 GPa serve as central strength members. They limit elongation during pulling and boost crush and bending resilience.

Water-blocking advances use swellable yarns and grease-free gel compounds to achieve near-complete moisture resistance. These measures protect optical paths and raise in-service reliability for cable installations in challenging environments.

These precision engineering steps integrate directly into fiber optic cable manufacturing workflows. When the production line aligns glass, coating, and mechanical specs, attenuation falls and networks gain reliability. That alignment shortens time to service for operators deploying modern broadband and high-speed internet technology.

Quality Control 4.0 And AI-Powered Inspection

Smart factories for fiber optic cable production now embed inspection systems that run continuously. These systems combine machine vision, machine learning, and automated testers to watch every reel and spool. The result is tighter feedback during the fiber optic cable production process and fewer surprises in the field.

AI models score coating uniformity, microbends, and surface defects at line speed. They cross-reference process telemetry from fiber optic cable production machinery and predict deviations hours before a reel moves to final spooling. This allows for in-line adjustments without stopping the line.

Automated OTDR integration performs 100% attenuation testing on every length. Modern OTDR systems using 1550nm sources map loss across reels and flag changes as small as 0.01 dB/km. Inline OTDR logs feed edge analytics for rapid root-cause tracing when a batch shows anomalies.

Robotic bend-radius simulators apply repeated stress cycles while monitoring macrobend loss. These testers validate compliance with ITU-T G.657 and customer bend specifications by running controlled bends at multiples of the cable diameter. Test outcomes are tied to batch IDs for traceability.

Thermal cycling chambers stress jackets and splices across wide temperature ranges. Environmental tests up to +85°C and down to -60°C confirm stability for extreme climates. Automated logs record each chamber run and link results to production lots.

Quality control 4.0 reduces returns and field failures by making 100% in-line testing routine. Edge analytics and OTDR integration shorten diagnosis times and improve regulatory compliance. Broadband operators see fewer truck rolls and better lifecycle performance for FTTH networks.

Cable Design Innovations For FTTH Deployments

New cable designs address common field challenges in fiber to the home technology. Engineers focus on durability, space economy, and speed of activation. These trends reduce installation time and lower long-term operational costs.

Bend-Insensitive Fiber Benefits For MDUs And Tight Routing

Bend-insensitive fiber maintains signal strength when routed around corners and through confined spaces. ITU-T G.657 compliant fibers minimize attenuation at tight radii, protecting links in multi-dwelling units and behind baseboards. Prysmian’s BendBright family and BendBrightXS exemplify how smaller coated diameters facilitate routing without compromising optical performance.

Flat Drop And Microcable Options For Flexible Deployments

Flat drop cable remains a preferred choice for aerial self-support, duct installs, and direct burial in North America. Its profile accommodates narrow pathways and enhances aerial spans with appropriate clamps. High-fiber-count flat drops necessitate enhanced radial strength and more robust hardware for longer spans.

Microcable technologies reduce outside plant profiles to 8 mm or less. Microcables and air-blown systems enable capacity addition inside existing ducts and congested corridors. These approaches reduce civil works, lower labor costs, and facilitate incremental network growth for urban and campus builds.

Pre-Connectorized Solutions To Speed Field Activation

Pre-connectorized solutions offer factory-terminated, plug-and-play assemblies that minimize field fusion and connector errors. Hardened outdoor connectors and vendor offerings like Prysmian’s ezDROP simplify mass rollouts and enhance first-pass yield. Service teams experience fewer truck rolls and faster service turn-up for smart city and 5G edge projects.

Cable Design Main Benefit Common Use Case Key Deployment Consideration
Bend-insensitive fiber Reliable operation at tight bend radii MDUs, indoor routes, mini-pathways Select ITU-T G.657 variants for indoor runs
Flat drop cable Versatile installation modes Aerial drops, buried runs, and duct insertion Use correct clamps and hardware for radial strength
Microcable systems Minimal footprint, incremental capacity Microduct installs, congested urban ducts Air-blown systems need compatible blower tools
Factory-connectorized solutions Faster field activation and fewer errors Mass deployments, rapid service turn-up Prepare for standardized connector interfaces

Sustainability And Energy Efficiency In Production Lines

Manufacturers in the fiber optic cable industry are embracing greener practices to reduce costs and meet consumer demands. Facilities prioritizing sustainable production witness improvements in operational efficiency and brand reputation. These advancements impact power systems, cooling, raw materials, and waste management.

Recovered energy systems strategies are becoming prevalent on extrusion lines and take-up reels. Regenerative braking on motor-driven spools returns power to the grid, thereby lowering net consumption. Studies indicate that energy recovery can reduce drive energy use by up to 32 percent in retrofitted reels.

Closed-loop cooling and chiller-less extrusion systems are reducing water demand. Adiabatic cooling can decrease water use by as much as 75 percent, particularly beneficial in water-scarce areas. Plants employing closed-loop cooling systems, in conjunction with heat exchangers, maintain temperature control while reducing utility expenses.

Recyclable jacket materials are transforming the disposal of cables. New polypropylene-based and modified polymer compounds meet mechanical and fire-safety standards, enabling higher recycling rates. Suppliers like Borealis and LyondellBasell are developing compounds that support the circular economy in cable jackets.

Process optimization minimizes scrap before recycling. Precision extrusion, in-line laser measurement, and real-time analytics reduce off-spec runs. Digital twins enable engineers to refine parameters, enhancing batch yields and reducing material waste.

Regulatory pressures and corporate ESG goals are compelling operators to favor vendors with transparent sustainability metrics. Municipal procurement teams and large network operators increasingly consider lifecycle impacts when selecting suppliers.

Operational Area Typical Gain Key Benefit
Regenerative drives on take-up reels Up to 32% energy reduction Lower power costs and less peak demand
Adiabatic and closed-loop cooling systems Approximately 75% reduction in water use Reduced water costs and easier compliance in dry regions
Recyclable cable jacket materials Higher post-consumer recycling rates Improved circularity and easier end-of-life handling
In-line inspection and digital twins Noticeable double-digit reductions in scrap and off-spec output Higher yield and lower material waste
Sustainability reports and certifications Improved procurement positioning Stronger appeal to network operators

Implementing these measures enhances the resilience of fiber optic cable manufacturing. It leads to lower lifecycle costs and easier compliance. Manufacturers integrating energy recovery and recyclable jacket materials position themselves for growth in the green procurement market.

Emerging Technologies Shaping Cable Manufacturing

New technologies are transforming the design and operation of fiber optic cable production machinery. These innovations expedite commissioning, diminish prototyping cycles, and empower manufacturers to test process alterations without halting production.

Digital twins create virtual replicas of entire production lines and novel cable designs. Engineers at Corning and Prysmian leverage these models to validate footprint, material flow, and layout before physical construction. Studies indicate commissioning can be up to 60% swifter when teams execute virtual scenarios and optimize layouts beforehand.

Digital twins facilitate expedited R&D for bespoke items such as armored variants and anti-rodent jackets. Virtual testing minimizes the necessity for physical prototypes and accelerates market entry. Teams can simulate process modifications, observe material interactions, and refine equipment parameters in a risk-free milieu.

AI systems introduce predictive capabilities on the factory floor. Machine learning scrutinizes 50+ parameters to forecast failures and quality deviations hours in advance. This AI predictive maintenance lessens unplanned downtime and elevates overall equipment effectiveness for high-volume lines.

Manufacturers like Siemens and ABB integrate AI with edge computing, enabling models to operate proximal to machines. Alerts prompt targeted inspections, spare part staging, and corrective actions before a fault halts production. This strategy maintains yield and shortens mean time to repair.

Quantum fiber sensing and distributed monitoring extend capabilities beyond production to the deployed cable. Embedded Brillouin and distributed acoustic sensing provide continuous strain and temperature data across extensive spans.

Integration of quantum fiber sensing enhances network diagnostics and supports structural health monitoring. Field teams acquire actionable insights when sensing data is linked to manufacturing records and test logs. This connection enables tracing anomalies to specific production batches.

Combined workflows—digital twins plus AI predictive maintenance—accelerate both commissioning and product development. Manufacturers embracing these tools can respond more swiftly to market fluctuations and deliver higher-value, differentiated cables.

Market-Driven Production Adaptations And Regional Needs

The global demand for fiber access compels manufacturers to adapt their production lines to local requirements. Regional fiber optic cable manufacturing now emphasizes durability, density, and safety. Plants employ modular equipment, enabling swift transitions between product families and meeting specific operator needs without significant delays.

In North America, networks predominantly opt for aerial routes and robust outside-plant solutions. Producers concentrate on creating armored aerial cables with enhanced breaking strength, corrosion-resistant armor, and simplified pole-mount installation. These designs withstand wind, ice, and long span stresses typical of utility corridors.

North American Priorities: Aerial And Armored Designs

Armored aerial cables are engineered for enduring reliability on poles and open spans. They boast 1,200 lb or greater tensile ratings and integrated steel or aluminum armoring to safeguard fibers against mechanical damage. Manufacturers deploy modular armoring units and rapid testing rigs, enabling mass production of these variants.

APAC And Europe: High-Density Microcables And Regulatory Compliance

In APAC, the scarcity of space and the need for dense builds drive demand for high-density microcables. These cables feature compact stranding towers and reduced-diameter fiber stacks, allowing for more fibers per duct. They significantly reduce civil costs by facilitating quicker overbuilds and easier microtrenching.

Europe mandates strict regulatory compliance for buildings and public spaces. Producers offer halogen-free, flame-retardant jackets that meet CPR classes like B2ca. Compliance testing is integrated into production lines, ensuring products meet fire-safety rules for indoor and outdoor applications promptly.

Across regions, the ability to adapt production is paramount. Compact stranding towers, modular extrusion and armoring units, and rapid prototyping enable factories to switch from armored aerial cables to microcable runs in mere hours. This flexibility allows operators to fulfill unique specifications while adhering to local codes.

Case Studies And Manufacturer Spotlight: Shanghai Weiye OFC Equipment

Shanghai Weiye OFC Equipment has solidified its reputation as a leading telecommunications equipment manufacturer. They cater to the FTTH and broader fiber markets. Their optical fiber cable equipment boasts advanced features, including SZ stranding, ribbon production, and extrusion with servo control. This ensures tight tolerances and high yields.

Their machinery for fiber optic cable production is equally impressive. It includes tape armoring units, automated take-up reels with regenerative drives, and integrated OTDR and vision inspection stations. These systems support various applications, such as bend-insensitive fiber, microcables, and pre-connectorized solutions. These are crucial for FTTH, 5G backhaul, and dense urban deployments.

Quality and sustainability are integral to their offerings. They employ OTDR testing, AI-powered inspection, and robotic bend simulators to meet QC 4.0 standards. Additionally, energy recovery options and closed-loop cooling reduce operating costs and scrap. Modular designs with AGV and edge computing support enable rapid reconfiguration and digital twin commissioning, catering to U.S. manufacturers and contract producers.

For operators in the United States, investing in Shanghai Weiye OFC Equipment can significantly enhance production capabilities. It ensures compliance with strict attenuation and mechanical specifications. This accelerates the introduction of new cable families, vital for broadband expansion. The company’s systems harmonize technical performance with practical manufacturing requirements.

FAQ

Q: What Advances Define Modern FTTH Cable Production Line Technology?

A: Modern FTTH cable production lines integrate high-precision mechanical systems with servo-driven extrusion. They utilize SZ stranding and ribbon machines, along with automated take-up reels. These systems also include integrated OTDR and AI-driven vision inspection, PLC orchestration, AGV material handling, and edge computing. Such advancements enable micron-level tension control and ±0.02mm jacket thickness tolerances. They achieve 95%+ automation and 100% in-line testing, reducing attenuation, scrap, and time-to-market.

Q: How Do You Define The Scope Of FTTH Cable Production Line Technology?

A: FTTH cable production line technology includes the machinery, process controls, and materials for fiber-to-the-home networks. It includes optical fiber drawing and coating, SZ stranding, and ribbon formation. Extrusion of inner and outer jackets, armoring or taping modules, and automated take-up and drum handling are also part of it. In-line optical and mechanical testing, along with the software stack—PLCs, edge servers, and industrial IoT—are integral to the process.

Q: Why Does Production-Line Quality Matter For Broadband Network Infrastructure?

A: Production-line quality directly impacts attenuation, splice loss, mechanical robustness, and long-term reliability. High-precision manufacturing minimizes intrinsic and macrobending losses. It extends reach, lowers field interventions, and improves first-pass yields. For carriers and ISPs, this translates to fewer truck rolls, lower total cost of ownership, and higher service availability for high-speed internet, 5G backhaul, and symmetrical multi-gigabit home services.

Q: What Role Do PLCs And Smart Machinery Play In Industry 4.0 Production Lines?

A: Programmable logic controllers (PLCs) provide deterministic synchronization across SZ stranding, ribbon forming, and take-up units. They enable sub-0.01mm tension precision, closed-loop extrusion control, automated recipe changes, and safety interlocks. When combined with robotic arms and automated armoring modules, PLCs form the backbone of Industry 4.0 production. They drive repeatability and high throughput with minimal human intervention.

Q: How Are AGVs And Edge Computing Used On Modern Cable Production Floors?

A: Laser-navigated AGVs move heavy drums and material spools with high positioning accuracy. Industry examples show 1,200kg capacity and sub-5cm placement. Edge computing processes terabytes of telemetry locally, delivering low-latency analytics and real-time quality alerts. Together, AGVs and edge computing improve material flow, reduce manual handling risks, and enable rapid correction of process deviations.

Q: What Precision Engineering Improvements Reduce Optical Attenuation?

A: Improvements include ultra-low-loss (ULL) glass formulations and advanced UV-cured acrylate coatings. These coatings cut microbending losses. Smaller coated diameters (e.g., 160–180µm) enable denser cable designs. Tight control of drawing tension, coating cure profiles, and extrusion concentricity—monitored by laser micrometers and closed-loop controls—lowers intrinsic loss and fluctuation across production reels.

Q: How Do Central Strength Members And Mechanical Design Affect Cable Performance?

A: Mechanical designs incorporating fiber-reinforced plastic (FRP) rods or high-strength central members control elongation during installation. They resist crush and bending, protecting fiber glass from strain. Proper selection of strength elements and buffer constructions reduces installation-induced loss, improves long-term reliability, and supports aerial or duct deployments with demanding mechanical requirements.

Q: What Does “QC 4.0” Mean And How Is It Implemented?

A: QC 4.0 describes a fully instrumented, data-driven quality-control regime. It includes 100% in-line testing, AI-powered vision inspection, automated OTDR mapping, robotic bend tests, and environmental chambers integrated into the production workflow. Edge analytics, traceable test logs, and predictive models enable rapid root-cause analysis, minimize returns, and ensure compliance with ITU-T and operator specifications.

Q: How Is OTDR Testing Integrated Into Production And What Sensitivity Can It Achieve?

A: Automated OTDR stations are integrated inline or at take-up to perform full-length attenuation mapping. They use dual-wavelength sources (including 1550nm). Modern setups can detect variations down to 0.01 dB/km, map localized defects, and tie results to batch IDs for traceability. This enables manufacturers to flag and quarantine reels before shipment, improving field reliability.

Q: What Are Robotic Bend-Radius Simulators And Thermal Cycling Chambers Used For?

A: Robotic bend-radius simulators apply repeated controlled bends and record macrobend loss to verify compliance with ITU-T G.657 and customer specs. Thermal cycling chambers run jackets and assemblies through −60°C to +85°C cycles to validate dimensional stability, jacket adhesion, and splice performance under extremes. Automated test logs provide traceable evidence for operator and regulatory requirements.

Q: What Cable Design Innovations Are Most Relevant To FTTH Deployments?

A: Key innovations include bend-insensitive fiber (BIF) for tight routing in MDUs and indoor paths. Flat drop and high-fiber-count flat assemblies are used for aerial and direct-burial North American use cases. Microcables and air-blown systems are for duct-constrained environments. Pre-connectorized assemblies speed field activation and reduce termination errors.

Q: Why Is Bend-Insensitive Fiber Important For MDUs And Tight Routing?

A: Bend-insensitive fiber maintains low loss under tight radii and repeated handling. It is crucial in multi-dwelling units, plenum runs, and behind baseboards. ITU-T G.657-compliant fibers help prevent macrobending loss during installation and reduce service calls related to routing-induced degradation. They support denser routing with fewer installation constraints.

Q: How Do Flat Drop Cables And Microcables Differ In Deployment Benefits?

A: Flat drop cables offer flexible aerial and direct-burial deployment with compact profiles suited to service drops. Microcables (≤8mm) and microduct systems excel in congested ducts and enable incremental capacity growth via air-blown installation. Choice depends on regional deployment practice, span requirements, and operator preferences.

Q: What Advantages Do Pre-Connectorized Solutions Provide?

A: Factory-terminated, hardened pre-connectorized assemblies reduce field splicing, eliminate human termination variability, and speed up service activation. They improve first-pass yield. Products like hardened OptiTap-style connectors and vendor pre-terminated drops support rapid mass-deployment strategies and lower workforce training needs.

Q: How Are Energy Recovery And Cooling Innovations Improving Sustainability?

A: Regenerative drives on take-up reels and motor assemblies can capture braking energy, reducing net consumption by industry-reported amounts (example: up to ~32%). Chiller-less or adiabatic extrusion cooling reduces water use by up to 75%. These measures lower operational cost, reduce water consumption, and align production with corporate sustainability targets.

Q: Are Recyclable Jacket Materials And Waste Reduction Practical For Production?

A: Yes. Recyclable compounds such as specially formulated polypropylene-based jackets can meet mechanical and flame performance while improving end-of-life recycling. Precision extrusion and in-line inspection reduce scrap rates. Combined with material-efficient tooling and digital-twin optimization, manufacturers can materially lower waste and support circular-economy goals.

Q: What Role Do Digital Twins Play In Cable Manufacturing?

A: Digital twins create virtual replicas of production lines and cable designs to simulate process changes and validate material flow. They accelerate commissioning. Industry estimates show commissioning and prototyping time reduced significantly (case examples up to ~60%). Digital twins also support offline testing of recipe changes and faster roll-out of new product families.

Q: How Does AI Enable Predictive Maintenance And Quality Prediction?

A: Machine learning models trained on dozens of production parameters can forecast equipment faults hours in advance and predict quality drift. Predictive maintenance reduces unplanned downtime, improves OEE, and allows planned service windows. AI-driven quality models provide early alerts for deviations that would otherwise produce rejects or field failures.

Q: What Is The Significance Of Quantum And Distributed Sensing Integration In Cables?

A: Embedding distributed sensing capabilities—such as Brillouin-based strain sensing and distributed acoustic sensing (DAS)—adds network-level telemetry for structural health monitoring, intrusion detection, and environmental diagnostics. Integrating sensing into cable designs enables added-value services and improved operational visibility for carriers and critical infrastructure owners.

Q: How Do Production Lines Adapt To Regional Market Needs (North America, APAC, Europe)?

A: Lines are modular and reconfigurable to meet regional priorities. North America focuses on robust aerial and armored designs with higher breaking-strength requirements for pole deployments. APAC emphasizes high-density microcables and compact stranding for dense urban rollouts. Europe prioritizes halogen-free flame-retardant jackets and CPR fire-class compliance. Modular stranding towers, quick-change extrusion heads, and configurable armoring units enable fast changeovers.

Q: What Manufacturing Equipment Is Essential To Support Varied FTTH Product Families?

A: Essential equipment includes SZ stranding machines (dozens to hundreds of fibers with micron-level tension control), ribbonization lines, servo-driven extruders with laser micrometers, tape or armor-wrapping stations, automated take-up reels with regenerative drives, inline OTDR and AI vision inspection, AGV drum handling, and edge computing/PLC orchestration for Industry 4.0 integration.

Q: How Do Manufacturers Ensure Compliance With Standards Like ITU-T G.657 And Regional Safety Codes?

A: Compliance is ensured via precise material selection (bend-insensitive fiber types), controlled production recipes, automated in-line tests (OTDR, macrobend testers), and environmental qualification (thermal cycling, flame tests). Traceable test logs, batch IDs, and documented QC protocols align production outputs with ITU-T recommendations and regional regulations such as CPR classifications in Europe.

Q: What Benefits Can U.S. Manufacturers Expect From Equipment Suppliers Like Shanghai Weiye OFC Equipment?

A: Suppliers like Shanghai Weiye provide modular, Industry 4.0-ready production machinery—SZ stranding, ribbon lines, precision extrusion with closed-loop controls, AI inspection modules, and integrated OTDR testing. This enables U.S. contract manufacturers and in-house producers to scale FTTH output, maintain tight attenuation and mechanical tolerances, adopt sustainability options (energy recovery, closed-loop cooling), and shorten time-to-market for variants such as armored aerial, flat drop, microcable, and pre-connectorized assemblies.

Q: How Do In-Line AI Inspection Systems Detect Subtle Defects At Production Speed?

A: AI-powered machine vision inspects coating uniformity, surface defects, and microbends using high-resolution cameras and convolutional models trained on labeled defect libraries. Models correlate dozens of parameters—diameter variance, coating texture, micro-crack signatures—to predict deviations hours before they become out-of-spec reels. This enables automated rejection, parameter adjustment, and reduced downstream field failures.

Q: What Testing Sensitivity And Traceability Are Achievable For Attenuation And Mechanical Validation?

A: Modern production lines integrate automated OTDR systems capable of resolving 0.01 dB/km changes, robotic bend simulators for repeated macrobend stress testing, and thermal chambers for extreme environment validation. Test results are stored with batch and reel identifiers in edge or cloud databases, providing full traceability for operator acceptance, regulatory audits, and customer service diagnostics.

Q: How Do Production Innovations Translate Into Market Outcomes For Network Operators?

A: Innovations in manufacturing yield lower-loss fibers, denser cable designs, and factory-terminated assemblies that reduce installation time and errors. Operators benefit from higher service reliability, fewer truck rolls, lower lifecycle costs, and faster rollout of symmetrical multi-gigabit services. These outcomes support widespread FTTH adoption, 5G backhaul capacity, and scalable connectivity for smart cities and hyperscale data center interconnects.

Related: Compact Fiber Unit: Optimizing Telecommunications